Stancold
  • Products & Services
    • Food Facility Fit-Out
    • Cold Store Construction
    • Cleanroom Construction Solutions
    • Firewalls & Industrial Partitioning
  • Data Centres
  • Our Team
  • CSR
  • Case Studies
    • Pharma
    • Food Projects
    • Industrial Partitions
  • News
  • Blog
  • Contact Us
View All News Case Studies Testimonials Video Gallery

Battery Manufacturer Cleanroom

Lithium Battery Research

Stancold

Background:

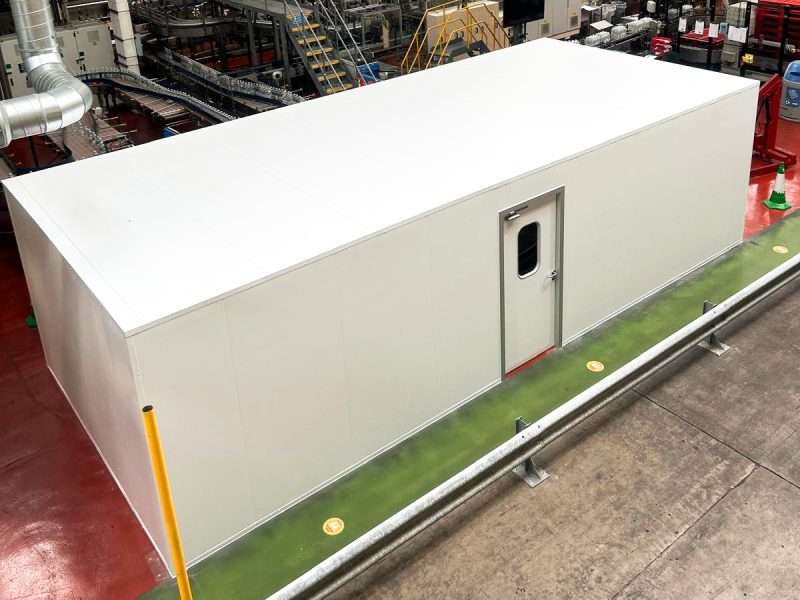
As a result of our expertise and bespoke cleanroom envelope packages, Stancold were awarded a new-build contract with a battery research organisation that specialises in reusing and recycling tin mining materials to create lithium batteries.

Process:

The client requested the new-build cleanroom as part of a pilot phase for a large-scale facility in the long-term.

Throughout the contract, the team collaborated closely with the manufacturing equipment contractor, who would later install the new machinery.

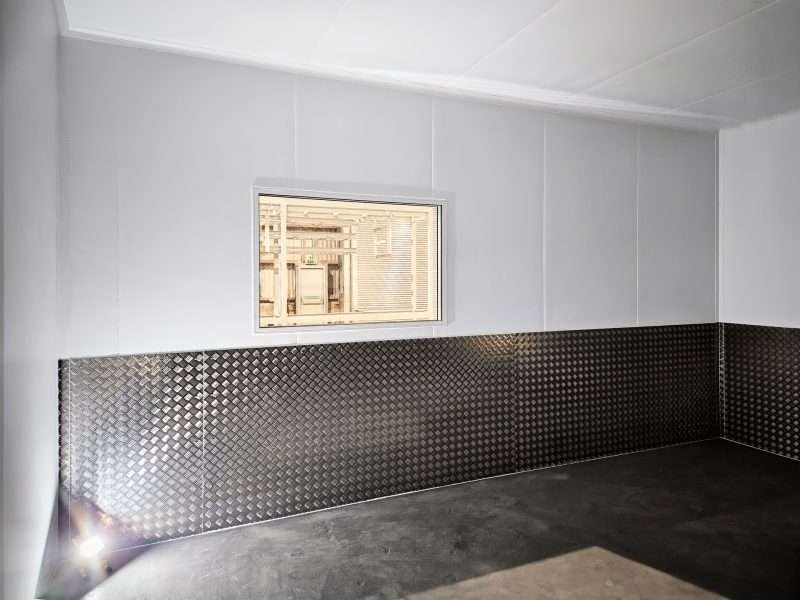
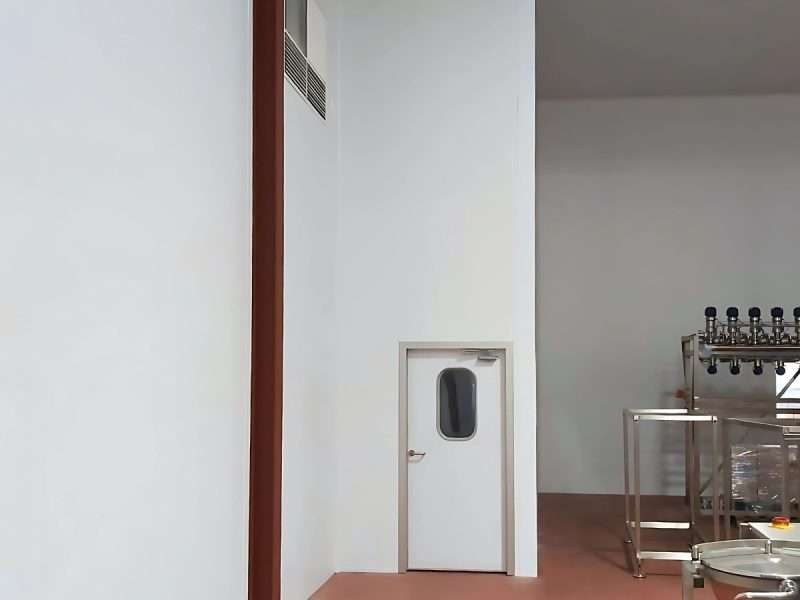
Included in the scope was the design and installation of double personnel doors for ease of access and a vision panel to enhance visibility within the facility.

Project Delivery:

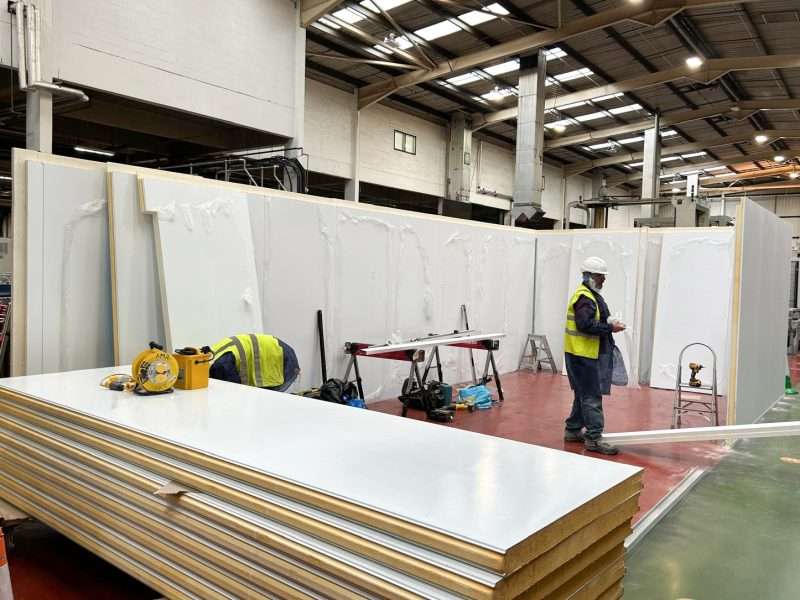
The team’s flexibility and proactive nature allowed them to build the initial walls during the first site visit, leaving a pre-designed opening to allow for the manufacturing equipment to be installed.

Due to the nature of the client’s work, a phased installation was required. The second phase began once the new equipment had been installed, resulting in the team returning to seal the room.

As per the client’s request, the team installed treadplate wall protection across the cleanroom perimeter in order to minimise the risk of potential damages.

The teams’ flexibility in this project left the client satisfied with the results.

Mark Kendrick, Business Development Director

More Info

Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY

Battery Manufacturer Cleanroom

Lithium Battery Research

University Cold Store Facility

Veterinary Anatomical Research

Stancold

The Brief

An M&E contractor already working with Stancold approached the team directly for the cold store scope within a university veterinary anatomical research facility in Bristol. The requirement was a dual-compartment chiller and freezer for the storage of equine cadavers, delivered inside a live, occupied campus building without interrupting scheduled teaching or research.

Our Approach

With refrigeration sitting within the contractor’s own scope, the envelope needed a specialist who could take it off their plate entirely – design, panel selection, access planning and installation – and return it complete and right first time. Several factors shaped delivery:

  • A live academic environment with scheduled classes and research continuing throughout
  • Delicate learning materials requiring careful relocation and securing before works began
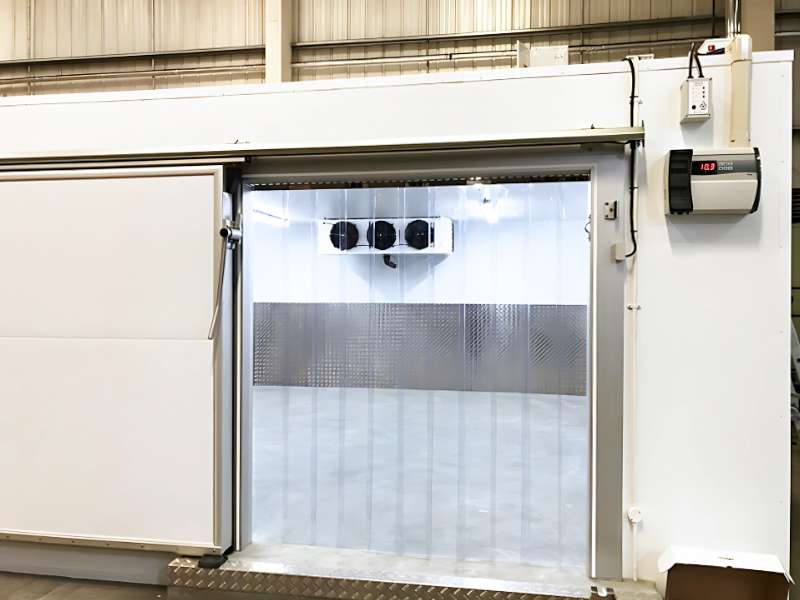
  • A dual-compartment chiller and freezer within one envelope, each with manual sliding doors for ease of access
  • Restricted site access and a working area to be secured and segregated from building users

The initial site survey was coordinated directly within the university’s timetable, allowing the programme to be agreed around their operations, rather than in conflict with them.

Delivery in Action

Kingspan QuadCore was utilised across the entire scope, at 80mm to the chiller and 125mm to the freezer, with 114m² of panelling forming both compartments and manual sliding doors to each.

Working within a secured construction area, the team integrated into the live building without disruption to academic activity, managing their own segregation, access and material movements so the contractor was not drawn into day-to-day coordination.

The installation was completed to specification and to programme, allowing the contractor to hand the facility back to the university without knock-on effect to scheduled teaching and research programme.

More Info

Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY

University Cold Store Facility

Veterinary Anatomical Research

N+1 Air Freight Storage Facilities

Air Freight Services

Stancold

Background:

Following the success of a prior project, CREST were contacted directly to help a pre-existing client design and build a coldstore, freezer, and ambient room for their second warehouse following a relocation.

Process:

The client required a fast turnaround, prompting CREST’s team to conduct a comprehensive site survey within just four days of the initial enquiry.

The scope of the project included the design of a bespoke reinforced freezer floor. Due to the nature of our client’s onsite operations, the traditional concrete flooring wouldn’t cope with the pressure from the excessive weight of the cargo pallets.

Our team’s strong communication and commitment to meeting client needs enabled us to deliver three high-quality designs, giving the client clear options to match their requirements.

Project Delivery:

Despite the tight schedule, the team were fully prepared to begin installation on-site within six weeks of the initial enquiry.

Due to the nature of the client’s work, the challenge of working in a live everchanging environment was presented. However, with the team’s extensive installation experience, the planning and delivery service ran smoothly.

Along with the bespoke freezer flooring, as part of the project scope we provided our N+1 refrigeration package that conducts constant temperature-mapping.

Our team worked incredibly hard in a live working environment.

Bob Stevenson, Senior Design Manager

More Info

Three Insulated Rooms
Three Insulated Rooms Inside Rooms
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Three Insulated Rooms

N+1 Air Freight Facility

Air Freight Services

Food Production Facility – Internal Fit-Out & Purpose-Built Extension, Birmingham

Speciality Food Manufacturer

Stancold

The Brief

Stancold were involved in early-stage negotiations with a growing speciality food wholesaler, who were looking to expand and relocate their manufacturing facility within Birmingham.

Experienced project management contractor, Pentadel, took on the full turnkey package to transform and extend an existing building into a fit-for-purpose food manufacturing facility.

Our Approach

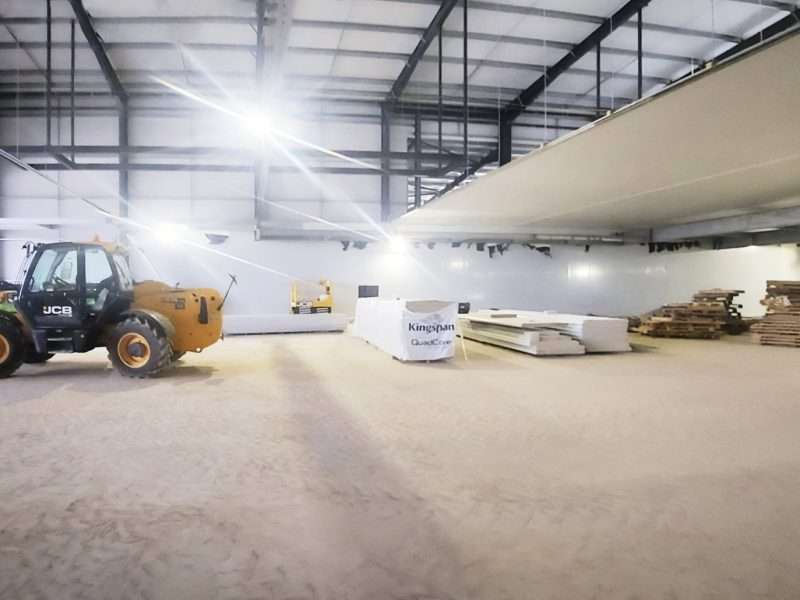
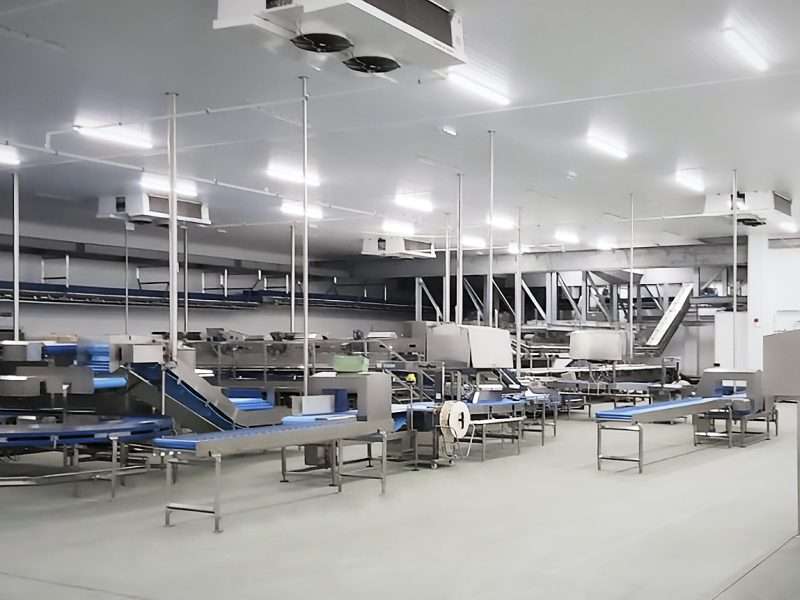
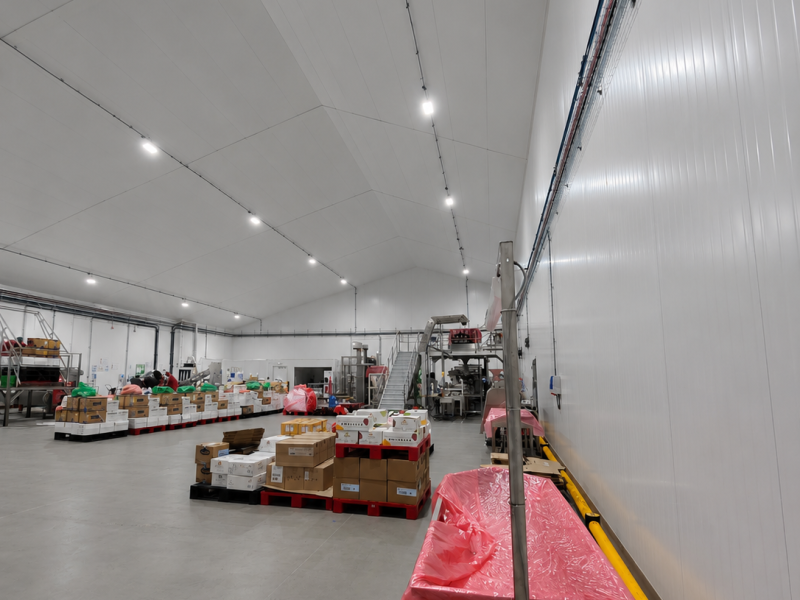
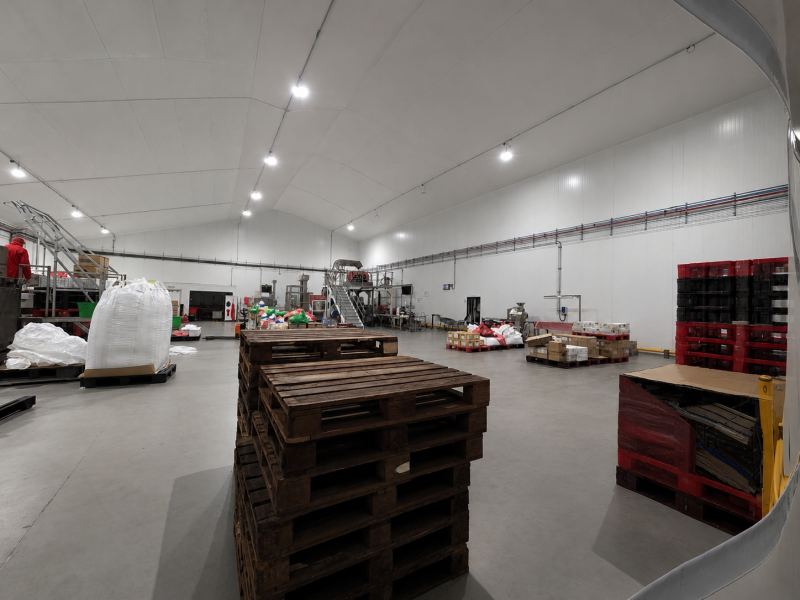
Stancold were appointed to undertake the food facility’s internal fit-out, alongside the internal and external cladding of a purpose-built extension, suited to product packaging and dispatch.

Our team worked collaboratively on the design and specification of this project to ensure that the end user’s requirements were met. Transferring specialist panel-build knowledge and skills into the external extension works allowed us to confidently add this element to our responsibilities.

The full specification included over 10 different areas, such as main production, a blast chiller, a dry store and a soy room.

Delivery in Action

As part of a 9-month phased construction, which included coordinating with other contractors on the busy site, Stancold successfully completed the hygienic panel installation to form areas as per the end user’s specification, alongside a 60-minute sub-dividing firewall between the building and its new extension, another part of Stancold’s scope to meet fire safety building regulations.

The internal fit-out extension construction included all cladding, using goosewing grey trapezoidal panels from Kingspan’s roof system, and door canopy. These works also encompassed a one-hour fire-rated boundary wall, utilising a RockSpan composite core. With tight access to consider, panels were craned from a bank to the rear of the building, alongside narrow plant used throughout.

Internally, the fit-out incorporated bespoke window details to accommodate the building’s existing roof lights, as well as specialist flush windows, allowing free viewing into the main production area. The team constructed a bulkhead to neatly conceal air handling equipment and all existing steelwork was encased to maintain food safety excellence.

This was a large project that required timely planning and coordination at every stage, where our team thrived in demonstrating such qualities.

You can take a tour around the facility here.

A project that demonstrated our commitment to the food industry

Sam Glover, Contracts Manager

More Info

Food manufacturing facility fit-out
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Food manufacturing facility fit-out

Food Production Facility

Speciality Food Manufacturer

Temperature-Controlled Marshalling Area for Large Food Distribution Hub, Coventry

ISS Property

Stancold

The Brief

After a glowing client recommendation, Stancold teamed up with ISS Property, experts in commercial property, to design and build a state-of-the-art chilled marshalling area within a bustling food distribution hub in Coventry. With the new end-user recently acquiring the site, they were eager to make key upgrades to optimise the space for their operational needs.

Our Approach

The marshalling area serves as a vital hub where products are inspected and sorted after being picked from the chilled warehouse, before seamlessly transitioning into delivery vehicles. Stancold’s extensive technical expertise came into play, allowing us to create solutions perfectly aligned with the end user’s operational requirements.

Delivery in Action

Stancold’s expert in-house installation team brought the chilled marshalling area to life using the Kingspan QuadCore composite panel system. The project featured a complex ceiling design to accommodate a fire suppression sprinkler system, seamlessly integrating the client’s existing sectional doors while installing state-of-the-art rapid-rise freezer and chiller doors, along with vision panels for enhanced functionality.

Delivered in just six weeks, this project moved swiftly from initial enquiry to handover. Drawing on over 75 years of expertise in the food and drink sector, Stancold ensured a high-quality, tailored solution that met the client’s needs with precision and efficiency.

Great work from the team across this successful 6-week installation

Lee Duffield, Stancold Project Manager

More Info

Temperature Controlled Marshalling Area; food manufacturing factories; Chilled Warehouse Construction; business models
Temperature Controlled Marshalling Area; food manufacturing factories; Chilled Warehouse Construction; business models Hygienic panels for food distribution hub
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Temperature Controlled Marshalling Area; food manufacturing factories; Chilled Warehouse Construction; business models

Chilled Marshalling Area

ISS Property

Dual-Compartment Freezer Build for Facility Extension

Dairy Producer

Stancold

Background 

Stancold was commissioned by a returning client, a Somerset dairy producer, to outfit a new facility extension with a dual compartment freezer to support growing production.

Although we complete projects nationwide, projects for food and beverage producers in our region carry extra meaning!

With the producer’s Managing Director overseeing the freezer build, we had to integrate smoothly with the end user and their multiple contractors.

Process

Our team carried out a site visit to map the extension and how it would tie into the existing facility, then worked through several design revisions to align with the client’s budget and wider extension plans.

To align with the extension’s pitched roof, the producer requested a matching pitched ceiling for the freezer, meaning panels for three of the walls had to be cut to precise slopes. As Stancold’s insulated panel packages are made-to-order, this was no issue for our project delivery team.

Our client opted to build a two compartment frozen storage area so one side can be shut down during low demand periods, reducing energy use, operating costs and their overall carbon footprint.

Project Delivery

Stancold coordinated with the dairy producer’s other contractors to construct the dual-compartment freezer space within their newly built extension using a bespoke system of 150mm Kingspan Quadcore panels. The installation was complete with two sliding freezer doors for entry into both compartments and floor angle protection as forklift trucks will be used in the storage space.

Our project delivery team also managed the installation of a modular heating mat onto the extension’s concrete base and the concrete floor covering to accommodate forklift truck use. A galvanised steel top hat suspension system allowed the pitched ceiling to be supported.

We are always pleased to use our extensive expertise of insulated panel systems to help a UK food or beverage producer expand their operations.

The pitched roof meant that the panels would need to be cut to a specific slope, but that was no issue for our installation team.

Rhys Morgan, Project Manager, Stancold

More Info

freezer build
freezer build freezer build freezer build freezer build freezer build freezer build freezer build
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
freezer build

Dual-Compartment Freezer Build

Dairy Producer

Freezer, Chiller & Distribution Centre, Gloucestershire

Newberry International

Stancold

The Brief

Newberry International Produce, a supplier and distributor, sought to build a factory in Gloucestershire, just up the road from us, to streamline their UK distribution operations.

Our Approach

The scope of this turnkey fit-out project included the installation of all the necessary whitewall panelling for the new facility.

The facility was designed to include a cold store and freezer with mobile racking for stock storage, three chiller rooms for produce preparation, a packing room, and a loading dock with direct access to distribution channels.

Delivery in Action

The Stancold team oversaw every aspect of the build, from groundworks and the construction of the freezer and chiller rooms to coordinating the installation of refrigeration, flooring, lighting, and floor slabs with appropriate ramps.

Our installers also engineered and built a bespoke solution to accommodate a loading bay that provides direct access from outside the building into the freezer, handling a temperature difference of up to 60°C.

Co-ordinating multiple trades and the design of the mobile racking were the biggest challenges on this project. Fortunately, the expertise of our contractors and flexibility of the client meant the project went seamlessly.

Bob Bryant, Project Manager, Stancold

More Info

Hygienic composite panels for food distribution centre
Hygienic composite panels for food distribution centre Sliding chiller doors in cold storage installation project Inside the hygienic cold storage unit for food production Loading dock access for food production Doors and panels at food distribution centre
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Hygienic composite panels for food distribution centre

Distribution Centre

Newberry International

Beverage Processing Area Upgrade, Kegworth

Drinks Producer

Stancold

The Brief

Stancold’s long history of delivering successful projects at this bottled drinks producer’s Somerset site led to a recommendation to carry out further facility upgrade works at their Kegworth location. As a producer with multiple sites nationwide, their trust in Stancold’s expertise demonstrates the strength of this ongoing partnership.

Process

As part of the upgrade works, Stancold installed a system of hygienic partitions to create a process area, ingredients room, handwash station, and cold store. The project also required an airlock to connect the existing storage space with the new processing area.

Leveraging their expertise, Stancold’s specialists recommended materials and ancillaries that aligned with the evolving plans, while carefully scheduling the installation to coincide with the client’s dedicated shutdown period.

Project Delivery

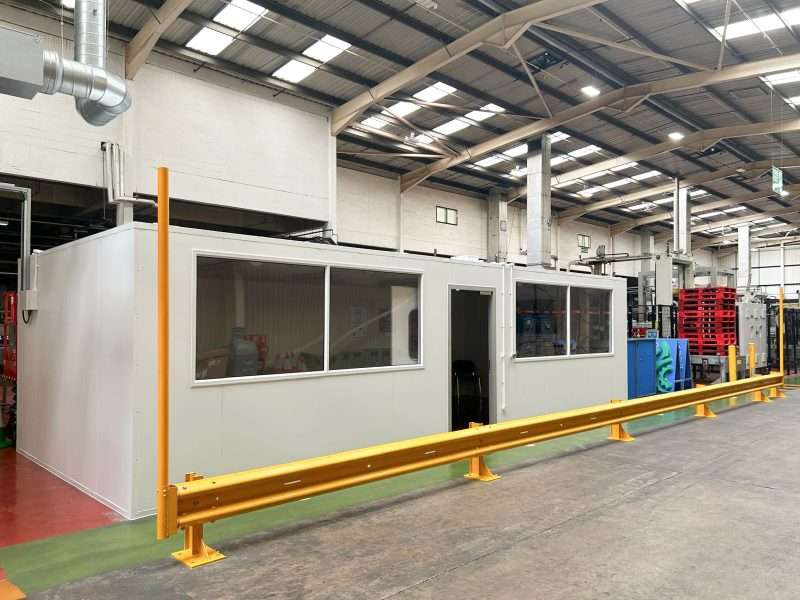
Stancold’s installation team successfully installed a large-scale partitioning system using the Kingspan Quadcore panel system, designed with a hygienic laminate finish. The project included multiple rapid rise doors, personnel doors, and large vision panels to ensure clear visibility between areas.

To ensure a seamless and professional finish, all exposed original steelwork was encased with white hygienic cladding, complementing the surrounding fit-out. Our installers showcased reliability and provided expert guidance throughout, successfully meeting the project’s design and specification requirements.

The whole team that installed the Kingspan walling, performed professionally throughout the project

Project Engineer, Drinks Producer

More Info

Food-Safe Partitioning; beverage processing area
Food-Safe Partitioning; beverage processing area Steelwork Cladding beverage processing Rapid Rise Doors Personnel Doors
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Food-Safe Partitioning; beverage processing area

Beverage Processing Upgrade

Drinks Producer

Abattoir Facility Fit-Out, Sheffield

Meat Producer

Stancold

The Brief

Stancold was approached by a principal contractor, working on behalf of a meat producer based in Sheffield, to fit out the producer’s abattoir facility.

Our Approach

Multiple whitewall partitioned areas were required to suit the end user’s operations, alongside a visitor gallery complete with vision panels for PPE-free abattoir viewing.

Project Delivery

Stancold were able to install the requested whitewall partitions and the viewing room adherent to the design agreed upon by all parties. The construction schedule was altered by the end user due to unforeseen circumstances, but we stayed on hand and were able to finish the project efficiently and thoroughly once they were ready for the installation to continue.

The project ended up requiring a complex system of hygienic whitewall panelling and over twenty specific door fit-outs. Despite the schedule alterations by the end user, Stancold made sure to see this installation through to the end, working with the main contractor and end user’s timelines. We were pleased to do our part in getting the abattoir up and running for the facility’s end user.

We were happy to accommodate the end user’s schedule to get this project completed.

Sam Glover - Stancold Project Manager

More Info

abattoir facility fit-out; brc audits
abattoir facility fit-out abattoir facility fit-out; brc audits abattoir abattoir facility fit-out abattoir facility fit-out
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
abattoir facility fit-out; brc audits

Abattoir Facility Fit-Out

Meat Producer

Production Area Fit-Out, Bodmin

Proper Cornish

Stancold

The Brief

As part of their continued expansion, Proper Cornish, winners of multiple Taste of the West Awards, needed to convert an engineering workshop space into a production area for a new product offering.

Stancold had previously delivered a freezer fit-out for Proper Cornish, and were thrilled to be invited back for the new project.

Our Approach

Our project specialists worked with Proper Cornish to finalise the layout and materials for a production space that would support every step of the manufacturing process, from raw goods to finished product.

The team worked diligently to complete the installation before Proper Cornish’s scheduled production kick-off.

Delivery in Action

The space was transformed by Stancold into a series of interconnected rooms, delivering a full-scope production facility tailored to Proper Cornish’s specific requirements and timeline.

The fit-out area was equipped to accommodate every stage of production, including a changing room for employees and a shared access space for both receiving raw materials and dispatching finished products.

The installation featured high-performance Kingspan Quadcore panels, fire-rated mineral fibre where needed, and a temperature controlled-space for product storage.

This marks another successful collaboration between Stancold and Proper Cornish. Our team looks forward to working with them again in the near future.

Thanks for your assistance in getting this prepared so quickly, you've set the bar high for your colleagues. We look forward to working with you again on another great project.

Adrian Wanless - Proper Cornish Project Manager

More Info

production area fit-out
production area fit-out production area fit-out production area fit-out production area fit-out production area fit-out production area fit-out
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
production area fit-out

Production Area Fit-Out

Proper Cornish

Hygienic & Fire-Rated Panels for Seafood Processing Facility, London

Seafood and Eat It!

Stancold

The Brief

Renowned for their excellence in project delivery within the seafood industry, Stancold was the natural choice for Seafood & Eat It!’s internal fit-out. The project demanded a comprehensive understanding of industry requirements and proactive, ongoing support from the earliest planning stages.

Our Approach

As the plans for the proposed mezzanine floor evolved, Stancold’s team collaborated closely with Seafood & Eat It! to ensure the industrial fit-out solution seamlessly aligned with the facility’s operational requirements.

The finalized layout featured a series of hygienic production rooms tailored to their new crab meat processing facility. This included frozen and chilled storage areas, a blast chiller and a dedicated office space to support their wider operations.

Delivery in Action

To safeguard the mezzanine floor, Stancold installed an independently suspended fire-rated ceiling, precisely fitted to the existing structure. Demonstrating flexibility throughout the project, the team also delivered a hygienic chiller area on the first floor, specifically designed for testing purposes.

Stancold’s unrivalled technical expertise in insulated and fire-rated composite panel systems ensured the project’s success from start to finish, with completion achieved in line with the main build programme.

A great example of our flexibility to changing plans and design.

Sam Glover, Contracts Manager, Stancold

More Info

Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY

Seafood Factory

Seafood and Eat It!

Phased Food Site Redevelopment, Wales

Minshall Construction

Stancold

The Brief

Stancold was appointed as the internal fit-out contractor by leading industrial construction company, Minshall Construction, as part of a food site redevelopment for an award-winning ingredients supplier in Wales.

Our Approach

Over a construction programme of three phases, Stancold were required to undertake the hygienic production fit-out of a new-build extension, the construction of a blast freezer and reconfiguration works to an existing production area.

The team were able to advise on appropriate design changes to suit the services already in place and navigate complexities around a large bulkhead section to the first floor.

Delivery in Action

Over 18 months, Stancold collaborated closely with Minshall Construction to complete the works in line with the scheduled programme, taking an approach that allowed the client to start operating in finished areas while others were still in progress.

Our package included the installation of both insulated and fire-rated composite panel systems, vision panels and doors to form high-risk and low-risk areas, airlocks and offices, all complete with a food-safe finish to fulfil the required safety standards and an aesthetically ‘clean’ fit-out throughout.

The team’s dedicated experience and understanding of constructing in live food manufacturing environments ensured that the delivery of this project met the end user’s expectations.

A food production facility transformed through this phased schedule of works

Sam Glover, Senior Contracts Manager

More Info

Food Production Facility Fit-Out; minshall construction; food site redevelopment
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Food Production Facility Fit-Out; minshall construction; food site redevelopment

Food Production Fit-Out

Minshall Construction

Cold Storage Build For Fresh Produce, London

Riverford Organic

Stancold

The Brief

As part of their exciting expansion plans, our client, Riverford Organic, called upon us again to assist in the construction of a cold storage area within their new distribution hub in central London.

Our Approach

As Riverford’s trusted supplier for hygienic panelling across their sites, Stancold collaborated closely with their Project Manager and the appointed refrigeration contractor to ensure the storage room met the required specifications for fresh produce while adhering to the agreed construction timeline.

Delivery in Action

Our team successfully installed the 120-pallet cold storage facility alongside 3 doors – a hinged chiller door, fire exit door and an automatic sliding chiller door.

Thanks to its superior insulating properties and white food-safe laminate finish, Kingspan’s Quadcore panel system was the most suitable option for these works, while the automatic sliding chiller door was chosen for access efficiency and convenience.

Our long-standing expertise in cold storage construction, spanning more than 75 years, is reflected in yet another successful project for a valued returning client.

It’s a pleasure to assist Riverford Organic as they continue to grow

Sam Glover, Senior Contracts Manager

More Info

Food-Safe Chiller; cold store
Food-Safe Chiller; cold store Kingspan Food Chiller Automatic Sliding Chiller Door
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Food-Safe Chiller; cold store

Food-Safe Cold Storage Facility

Riverford Organic

Turnkey Frozen & Chilled Storage Package

Speciality Foodservice Provider

Stancold

The Brief

Rising demand had pushed a South East foodservice provider beyond its existing cold storage capacity. As the first phase of a wider expansion plan, the business needed additional frozen and chilled storage within a newly acquired warehouse in Kent, operational quickly enough to meet that demand.

Our Approach

Stancold offered a full turnkey cold storage package, giving the client one partner to coordinate the build from empty warehouse to working facility. The scope covered insulated hygienic panelling, doors, racking, flooring and electrical connections, with refrigeration installed by the client’s nominated contractor.

Pre-construction meetings between all three parties resolved design details and the finer points of the build before work began on site. This kept responsibilities clear and the programme on track.

Delivery in Action

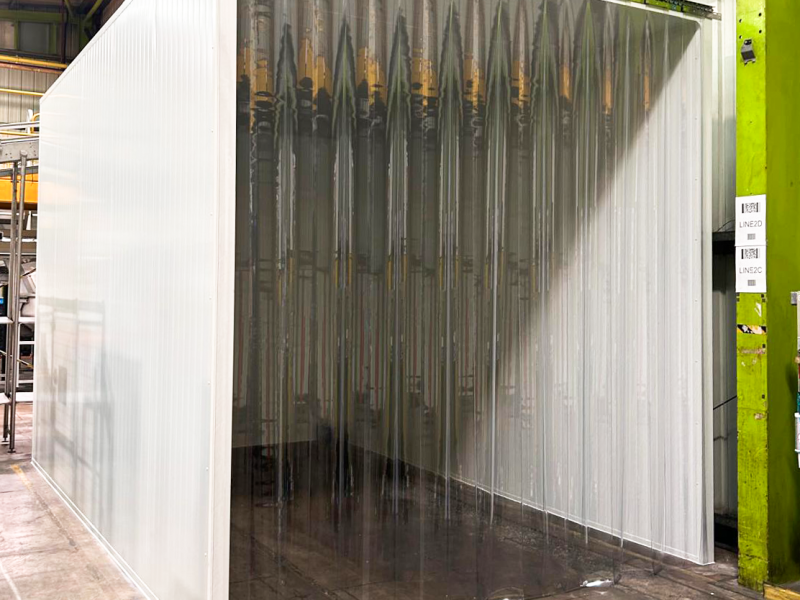
Kingspan QuadCore was used throughout: 150mm panels formed the large freezer and 100mm panels formed the chiller. Both have a smooth hygienic finish and are fitted with Kingspan sliding doors.

The team coordinated the freezer’s concrete flooring, heavy-duty pallet racking for 280 pallets, and integration of a refrigeration system capable of holding -18°C.

Completed in six weeks from order to handover, both spaces were fully operational and ready for immediate use. The client had the capacity in place to meet demand from day one, as the first step in its wider expansion.

Been a total pleasure working with you, can’t speak highly enough of your whole team, start to finish.

Foodservice General Manager

More Info

turnkey cold storage facility
turnkey cold storage facility Food-Safe Freezer; industrial freezer Food-Safe Chiller Food-Safe Chiller Strip Curtains and Sliding Freezer Door
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
turnkey cold storage facility

Frozen & Chilled Storage

Speciality Foodservice Provider

10,000m² Production & Storage Facility For Food-To-Go Manufacturer, London

Food-To-Go Manufacturer

Stancold

The Brief

Due to continued business growth, this food-to-go manufacturer needed to expand their food production and storage facility.

Our Approach

For this complex scheme, we had to consider the different temperatures for chillers, freezers and packing facilities along with fire-rated areas within the production facility. The plan included a range of facilities; ingredient chillers, product preparation rooms, temperature-controlled packing areas, low-temperature storage and marshalling areas, alongside the installation of 58 various doors.

Delivery in Action

To suit the requirements of each room, a range of different panel thicknesses were used across the project, including a 175mm firewall. Due to its large-scale nature, a project re-design was required during installation to include adaptations to work around steel walkways in the ceiling.

The complexity of this project displayed the Stancold team’s technical capabilities and ability to meet our clients’ specific requirements.

A large-scale complex project delivered exceptionally by the team

Lee Duffield, Project Manager, Stancold

More Info

Chilled Storage, London; production facility
Chilled Storage, London; production facility Storage Facility London Food Manufacturer Installation London
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Chilled Storage, London; production facility

10,000m² Storage Facility

Food-To-Go Manufacturer

Bacon Freezer, Bodmin

Proper Cornish

Stancold

The Brief

Nestled in the heart of the South West, Proper Cornish is a celebrated producer of baked savoury delights. With a rich heritage and an unwavering commitment to quality, they continue to craft their iconic products from their base in Bodmin. As a proud Cornwall-based producer, Proper Cornish champions the region’s culinary excellence.

Recently acquired by the Onore Group, the company is poised for even greater growth while staying true to its Cornwall roots. A new contract with a nationwide distributor marked an exciting milestone, necessitating an operational expansion. To support their growing production needs, Proper Cornish enlisted the expertise of the Stancold team to transform an unused space into a state-of-the-art freezer, specially designed to store bacon destined for their signature pastry goods.

Our Approach

The initial plans involved fitting whitewall around the facility’s columns. However, we proposed an alternative solution: fitting the whitewall across the columns instead. This approach not only reduced the overall project cost but also made no impact on the freezer’s storage capacity due to the size and shape of the good stored there.

Delivery in Action

The Stancold team successfully completed the installation of whitewall partitioning at Proper Cornish’s facility. The bacon freezer was built using Kingspan Quadcore panels for both the walls and ceiling, and featured a strip curtain along with an insulated concrete floor incorporating a modular heater mat, ensuring it aligned seamlessly with the existing facility’s floor level.

Collaborating with a renowned and longstanding South West food producer like Proper Cornish was a privilege for the team, who were thrilled to contribute to their continued success.

We look forward to working with you on another great project.

Adrian Wanless - Proper Cornish Project Manager

More Info

bacon freezer
bacon freezer bacon freezer bacon freezer
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
bacon freezer

Bacon Freezer

Proper Cornish

Co-op Temperature-Controlled Distribution Centre, Thurrock

The Co-operative

Stancold

The Brief

The Co-op, part of the Co-operative Group, operates nearly 1,800 food stores and is the UK’s leader in top-up food. Their brand is one of the most well-known in the UK, having existed in British communities since 1863.

Stancold has the flexibility to undertake projects of both a smaller scale for growing food producers and larger scale projects for extensive facilities of nationwide organisations such as the Co-op.

Our Approach

Co-op approached our team to enquire about building three specific temperature areas, chilled, frozen and ambient, for their new distribution facility in Thurrock. They also required specific office areas and a plant room as part of the wider scope of works.

This involved multiple site visits beforehand by our projects team and extensive communication with the client to determine the best layout and process for building the required areas.

Delivery in Action

Stancold was able to coordinate with the operations team at the Thurrock facility to efficiently build the required areas with minimal disruption to the facility’s operations. The project included the design, supply, and installation of composite insulated panels tailored to the client’s needs.

As part of the wider scope of works, we delivered chilled, ambient and freezer areas for the new distribution centre. The project was delivered efficiently and to the satisfaction of the client.

The Stancold team are proud to have had the opportunity to work with such a valued UK-based organisation and support their extensive distribution network!

It was a great experience getting to work with one of the UK's most recognisable organisations on this extensive project.

Andy Croxton, Stancold's Managing Director

More Info

composite insulated panels for co-op distribution centre
composite insulated panels for co-op distribution centre freezer area for distribution hub, cold room freezer area, cold room, chiller
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
composite insulated panels for co-op distribution centre

Distribution Centre

The Co-operative

Mixing Hall Fit-Out, Northamptonshire

Snack Producer

Stancold

The Brief

Stancold was approached by a UK manufacturer of dried fruit, nuts, and baking ingredients to convert existing warehouse space into a hygienic food production and temperature-controlled storage area.

Rising demand had left the business needing more room to expand its manufacturing operation within the existing facility

Our Approach

Our team worked with the customer to establish the suitable panel layout for the required production space and chilled storage area.

The whitewall panel package had to be designed around the pitched ceiling of the existing warehouse.

The mixing hall required a staff change point and wash area consistent with the hygienic standards of the space.

Delivery in Action

Stancold used the Kingspan Quadcore panel system to deliver the hygienic mixing hall, complete with a chilled storage space and change point, so the customer could add the additional production line.

The construction package included all required doors, with rapid rise doors fitted to both the production space and chiller for safe forklift access.

Rising demand with no room to grow is a familiar challenge - our bespoke whitewall panelling packages solve it.

Andy Connell, Business Development Manager

More Info

mixing hall
mixing hall
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
mixing hall

Mixing Hall Fit-Out

Snack Producer

Internal Storage Area and Production Briefing Area Fit-Out, Derby

Refresco

Stancold

The Brief

Stancold has worked on multiple installation projects for our the team at Refresco at their various sites. Our project specialists have developed a strong relationship with Refresco and they can always rely on Stancold to help their production facilities evolve and expand.

Our Approach

While we were planning out the installation of a storage area for packaging materials at Refresco’s Derby site, they came to us with an additional project for a production briefing area. This would make production meetings more efficient for the Refresco team as getting to the existing offices required a long walk through the factory.

Due to the fast-paced nature of their production operations, it was in the best interest of the client for us to get both projects completed within the same week.

Delivery in Action

To finish both projects within the same week, not only did our projects team have to alter the production schedule for the on-site installers, but the delivery of the panels for the office fit-out needed to be moved forward.

Having worked in live food production facilities for over 75 years, we are no strangers to shifting installation programmes. We were able to complete both the storage area and production briefing office installations to the highest quality and on the agreed-upon timescale for our friends at Refresco.

Our extensive installation experience put us in a position to be able to complete both installations with minimal disruption to the client’s operations.

Sam Glover - Project Service Manager

More Info

storage area; production briefing area
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
storage area; production briefing area

Storage Area & Office Fit-Out

Refresco

Hygienic Production Area Fit-Out, Chichester

Parkers Foodservice Ltd

Stancold

The Brief

To be able to expand their service offering across pubs, schools and hotels, family-run wholesaler Parkers Foodservice entrusted Stancold to assist in their relocation to larger premises in Chichester.

Our Approach

The new building required a hygienic production area fit-out, which included two freezers, three chillers and a preparation area. On the site survey, Stancold were able to offer advice on suitability for their needs and adapt the design accordingly.

Due to the existing structure of the premises and a mezzanine to work beneath, attention-to-detail was key throughout the design stages to accommodate expected intricacies during the install.

Delivery in Action

Stancold utilised Kingspan’s Quadcore hygienic panelling system to construct five temperature-controlled areas, two freezers and three chillers, alongside a prep area within the vacant space. The was accompanied by a number of sliding freezer and chiller doors to complete the fit-out.

The team carefully cladded all existing steel columns, working efficiently and flexibly as several design changes were made over the course of the installation.

The hygienic production area fit-out project was successfully completed in under three weeks, to the client’s specification and level of satisfaction.

A detailed installation successfully achieved by the team

Sam Glover, Project Manager

More Info

hygienic production area
hygienic production area Hygienic Production Fit-Out hygienic production area fit-out hygienic production area Food-Safe Prep Area hygienic production area hygienic production area
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
hygienic production area

Hygienic Production Fit-Out

Parkers Foodservice Ltd

New Dairy Factory, Blagdon

Yeo Valley

Stancold

The Brief

Yeo Valley is a family-run business based in Somerset, producing organic dairy products since the 1960s. Our team has worked with Yeo Valley on many occasions, establishing a great relationship between the two companies.

Our Approach

Stancold was appointed to expand the existing dairy factory to the client’s specifications, with two large production areas, hygienic corridors and a blast chiller area, overlaid by a large self-supporting ceiling. The partition between the existing factory and around the perimeter needed to be a 2-hour fire-rated wall.

Delivery in Action

From the preliminary design and feasibility stages, Stancold worked closely with the client to ensure all elements of the projects were considered. The project had to be carefully managed as we ‘broke through’ the live factory at several points, all of which we managed with ease.

Stancold were able to deliver the dairy factory fit-out on schedule and to Yeo Valley’s specifications.

You’ve done a fantastic job.

Joe Wharton - Yeo Valley

More Info

hygienic food safe corridors and a blast chiller area; dairy factory
hygienic food safe corridors and a blast chiller area; dairy factory hygienic food safe corridors and a blast chiller area hygienic food safe corridors and a blast chiller area hygienic food safe corridors and a blast chiller area
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
hygienic food safe corridors and a blast chiller area; dairy factory

New Dairy Factory

Yeo Valley

Hygienic Cheese Production Extension, Bath

Bath Soft Cheese

Stancold

The Brief

Stancold was pleased to continue its partnership with Bath Soft Cheese, a respected producer right around the corner from us, as we were once again approached to assist with their latest site expansion.

Our Approach

To expand its production capabilities, Bath Soft Cheese required a hygienic fit-out within its recently built extension, therefore creating new space for maturation and blue cheese production.

Delivery in Action

Our project delivery team installed a bespoke system of Kingspan Quadcore composite panelling to form six new areas within the production extension, integrating Mineral Fibre panels to comply with Building Control’s passive fire protection requirements.

The mezzanine floor was capped and clad to achieve a clean, visually appealing finish, while eight new doors were installed and two of the client’s existing doors were re-installed with care.

This project with Bath Soft Cheese was a great success. Even with COVID safety measures in place, our team ensured efficient delivery, value-engineered solutions, and a satisfied client.

Our team demonstrated efficiency and, of course, safety on this project

Sam Glover, Project Manager

More Info

New hygienic rooms for cheese production
New hygienic rooms for cheese production bath soft cheese Hygienic areas for cheese and dairy businesses
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
New hygienic rooms for cheese production

Cheese Production Extension

Bath Soft Cheese

Butchery Chiller & Meat Preparation Area, Nailsea

Bakers of Nailsea

Stancold

The Brief

Bakers of Nailsea is a family-owned butchery and abattoir located in North Somerset. With over 100 years of history, the business is dedicated to providing responsibly sourced, high-quality meat products to customers throughout Somerset and Devon.

The team at Bakers approached to Stancold to manage the installation of a bespoke system of composite panelling to facilitate their expanding operations.

Our Approach 

As a valued returning client, Bakers of Nailsea entrusted Stancold with the creation of a dual-compartment chiller and a production area, complete with an airlock system, to support the expansion of their operations.

This project highlights our ongoing commitment to supporting local food producers and strengthening the food supply chain in the Somerset and Devon regions. Our project delivery team carefully planned and scheduled the work to ensure that the existing operations continued seamlessly without disruption.

Delivery in Action

Stancold successfully installed a range of temperature-controlled areas, complete with refrigeration. This included a large freezer, five chill rooms for various food products, a food preparation area and marshalling areas. We also installed fire-rated office partitions over two levels.

We proudly handed over a fully equipped, state-of-the-art facility, meeting the agreed deadline and ready for immediate operation.

Brilliant product and installation. I found your Project Manager and whole team very easy to deal with.

James Baker, Bakers of Nailsea

More Info

butchery; food facility
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
butchery; food facility

Butchery & Abattoir

Bakers of Nailsea

Food-Safe Fit-Out in Production Extension for National Food Manufacturer, Slough

National Food Manufacturer

Stancold

The Brief

Following a competitive tender process, Stancold won the work to complete the entire internal food-safe fit-out for a new food production area extension spanning two floors, undertaken by national contractor, Walker Construction.

Our Approach

The end user, a household name in food manufacturing, specified non-combustibility as a key factor within the construction. To meet their requirements, Stancold were able to offer white hygienic panelling with a Mineral Fibre core and worked with Walker Construction and the end user to accommodate changing design specifications before starting on-site.

Delivery in Action

Stancold installed a comprehensive system of mineral fibre core panelling with a hygienic finish, to form a number of new areas within the vast production warehouse space. This included goods-in areas, pallet stores, stairwell enclosures between floors, hygienic corridors and plant rooms.

We were also responsible for the installation of all single and double fire exit doors, as well as 60-minute fire-rated doors where required; approximately 40 doors in total.

The team took care of the intricate construction details around the existing steelwork, carefully matching up panel joints for an aesthetically pleasing finish throughout. Our attention to detail and flexibility on-site, working with and around other contractors, were key elements in ensuring that the build was a success.

A large-scale fit-out project delivered exceptionally by the Stancold team

James Hoy, Contracts Manager

More Info

Food-safe factory fit-out, Slough; food production extension
Food-safe factory fit-out, Slough; food production extension Food-safe factory fit-out, Slough Food-safe factory fit-out, Slough Food-safe factory fit-out, Slough Food-safe factory fit-out, Slough Matching panel joints around steelwork
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
Food-safe factory fit-out, Slough; food production extension

Production Extension Fit-Out

National Food Manufacturer

Commercial Kitchen Build, Bristol

Easton Chilli

Stancold

The Brief

Easton Chilli was started by Rikki Tooley as a passion project and it quickly grew into a successful Bristol business. Initially operating out of rented and pub kitchens, Rikki soon outgrew those spaces. Discovering an available Easton unit, he needed a specialist contractor for a thorough, hygienic fit-out.

Our Approach

Rikki found Stancold through his membership in Taste of the West. Keen to support the growth of independent South West food producers, Stancold promptly collaborated with him to develop a kitchen fit-out that met his exact needs. The project scope for the production space also included the installation of two food-safe hinged personnel doors.

Project Delivery

The Stancold installation team efficiently completed a system of Kingspan Quadcore hygienic panelling to form Easton Chilli’s production space within their new industrial unit.

One logistical consideration was navigating Easton’s compact roads, which meant Stancold had to arrange for the panels to be delivered on smaller vehicles. In 75+ years of delivering food production fit-outs, that was far from a challenge for our team.

Stancold delivered the commercial kitchen fit-out on time and to the exact specification of the client, so that Easton Chilli could commence producing their excellent chilli jams and sauces.

Installation process itself was efficient and done well.

Rikki Tooley - Founder of Easton Chilli

More Info

commercial kitchen
commercial kitchen
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
commercial kitchen

Commercial Kitchen Build

Easton Chilli

New Bakery Fit-Out, Somerset

Artisan Bakery

Stancold

The Brief

An artisan bakery based in Somerset partnered with the Stancold to build a new bakery production facility, supporting their plans to expand operations and meet growing demand for their baked goods.

We thoroughly enjoyed the opportunity to work with a local food producer, especially one so passionate about their craft. Supporting the food and drink industry is something we take great pride in, and it’s always rewarding to play a part in helping businesses in our region grow and thrive.

Our Approach

Our team worked closely with the bakery’s management to create a practical and efficient layout for their new facility. This included a walk-in freezer, chiller store, hygienic storage and production areas, as well as changing rooms and a stairwell spanning two levels.

Stancold’s experienced project managers collaborated with the client to ensure the site’s whitewall layout was tailored to support smooth and efficient day-to-day operations.

Delivery in Action

Stancold’s team worked seamlessly with the appointed builders to install the required whitewall partitions and cold store solutions, ensuring the project met the agreed timelines for both the client and other contractors involved.

The installation included the required system of whitewall panelling in three different thicknesses, along with PVC strip curtains, sliding chiller and freezer doors, a modular heating mat, and concrete flooring. Each element was carefully selected and installed to suit the client’s specific operational needs.

We’re proud to have played a role in supporting the South West’s thriving food and drink industry and look forward to continuing our work with local producers.

The whole job was very good and completed in the agreed timescale.

Michael P., Operations Director

More Info

Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY

New Bakery Build

Artisan Bakery

Drinks Production Site Offices, Manchester

Kingsland Drinks

Stancold

The Brief

Kingsland Drinks is a premier independent supplier of wine and spirits based in Manchester. They have been based in the UK since their founding in 1895 and distribute to a wide range of customers including Nisa, Co-Op, and Tesco.

Our Approach

Kingsland approached the Stancold team to install a triple-compartment office within their existing drinks production facility.

The project delivery team presented Kingsland with multiple designs with different layouts and worked with their site managers to settle on a design that would suit their needs and efficiently use the existing space in the facility.

We were able to work flexibly with the client’s changing timescales.

Delivery in Action

Over the course of the project, Stancold installed the triple-compartment office to the agreed specifications centring around the Kingspan Quadcore system.

As part of the office build, we also supplied and installed two capped openings, three single-hinged doors and two polycarbonate vision panels.

We were able to set up the office project to provide minimal disruptions to the client’s day-to-day drinks production operations.

This installation was efficient, thorough, and to the client’s satisfaction!

Sam Glover - Stancold Project Manager

More Info

drinks production site offices
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
drinks production site offices

Drinks Production Site Offices

Kingsland Drinks

Holding Freezer For Food Wholesale, Essex

Time Wholesale UK

Stancold

The Brief

Our client, Time Wholesale UK, approached us to provide a temperature-controlled facility for the storage of ice products at their site.

Our Approach

Stancold worked with the client and a trusted refrigeration partner to design a solution that would fit Time Wholesale UK’s temperature, food-safe and logistical needs.

The facility design needed to fit within the available space in the existing wholesale warehouse.

Delivery in Action

The team constructed a facility to suit the client’s specification with Kingspan Quadcore composite panels.

Aluminium treadplate protection was added to all internal walls in order to prevent damage from forklifts and pallet trucks.

A sliding freezer door, strip curtains and insulated concrete flooring were also installed as part of the project specification, where the timing and coordination of each element was key to ensure a successful build and a satisfied client.

The installation also accommodated a condenser unit to the rear of the room so that the entire facility could remain self-contained.

Another project successfully completed through our team's systematic approach

Sam Glover, Contracts Manager

More Info

holding freezer
holding freezer Food Service Freezer Holding Freezer holding freezer
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
holding freezer

Food-Safe Holding Freezer

Time Wholesale UK

Insulated Engineering Workshop for Dairy Producer, Wiltshire

Dairy Producer

Stancold

The Brief

A building contractor Stancold regularly works with contacted us to assist with a project at a Wiltshire dairy facility.

The dairy producer wanted to line their engineering workshop with hygienic whitewall panelling to match the rest of the facility and to insulate it against external temperatures. They also required the installation of an office space in the workshop for their engineers.

Food production sites often have an engineering workshop separate from the production and product storage areas. In many cases this is for the maintenance of site machinery.

Our Approach

The Stancold project delivery team collaborated with the main contractor and the end user to develop an optimal design for the engineering space.

The design had to account for an existing roller door in the engineering space.

Delivery in Action

Stancold efficiently installed the insulated engineering workshop and office space using Kingspan Quadcore panelling, ensuring it not only matched the rest of the facility but also provided improved warmth for the engineers during the colder months.

The design and installation also incorporated an opening for the existing roller door and two hinged personnel doors for staff access.

The nature of the panels serves to not only provide consistency with the rest of the site, but also insulate the engineers from external temperatures.

Andy Connell, Business Development Manager

More Info

insulated engineering workshop
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
insulated engineering workshop

Insulated Engineering Workshop

Dairy Producer

Savoury Fruits Processing Area, Crewkerne

Yeo Valley Organic

Stancold

The Brief

Yeo Valley is one of the UK’s premier dairy producers, operating four sites throughout the Southwest. Stancold has a strong working history with Yeo Valley of over twenty years, helping them with multiple builds and maintenance projects each year. We are proud to be their preferred fit-out partner.

Our Approach

The team at Yeo Valley approached us to design and build a new whitewalled processing area for their savoury fruit projects within an unused space at their Crewkerne facility, to be built on existing flooring.

Stancold’s team worked with the client to create a cost-efficient design for the processing facility over multiple revisions that met the client’s various requirements. Stancold’s installers would have to work around a drainage project in progress at the facility during the same timescale.

Delivery in Action

Stancold successfully delivered the processing area to Yeo Valley’s exact specifications within the required timeframe. This included installing high-performance Kingspan Quadcore paneling, capping openings for existing doors, fitting a new door, and suspending the ceiling from the existing structure.

Additionally, Stancold installed ceiling-mounted railings to ensure Yeo Valley’s team could safely carry out maintenance on the whitewalled roof.

Another successful project for our good friends at Yeo Valley!

Sam Glover, Senior Contracts Manager

More Info

yeo valley processing area
processing area yeo valley processing area
Previous Testimonial
Next Testimonial
SHARE
Linkedin Twitter Facebook
CASE STUDY
yeo valley processing area

Savoury Fruits Processing Area

Yeo Valley Organic

Load More
Loading

What Next?

Case Studies Our Team Architects' Zone

CONNECT WITH US

NEWSLETTER SIGN-UP

  • This field is for validation purposes and should be left unchanged.
  • I am interested in

Tweets by @Stancold_UK

OUR HISTORY

1946

Creation of Rowland Adams Metals Ltd, Bristol

A partnership between Mr Adams and Mr Rowland, two metalworker friends back from the war. Over the years, they became one of the first companies in England making cork filled coldroom panels that were sandwiched between timber frames and vapor repellent faces infilled with rope fibres, bitumen and caulk to create a seal.

Stancold 1946
1979

Name change to Stancold Coldstore Construction

Where the name originated from is a combination of urban legend and myth. Some say it was the idea of an installer called Stan, some say it was a “clever use” of the concept of 'Standing in the Cold'. However we got here, we are proud of our roots!

Stancold 1979
1988-1997

The Gillham family steps in

Mervyn Gillham came from a different field and saw the potential within Stancold to become a leading company in this specialist marketplace. In 1997, his son Kevin Gillham joins the team.

Stancold 1988-1997
1999

Stancold acquires Mercury Coldrooms

Stancold becomes one with the well reputed local coldstore business, Mercury Coldrooms, bringing a wealth of knowledge and a great team of people to the company. Today, the majority of the senior management team of Stancold and our top project managers are originally from Mercury.

Stancold 199
2000

New HQ

As a result of rapid expansion, Stancold moves into a new 2600 m² building conveniently located just off the M4 motorway in Avonmouth. This exciting change has allowed us to consolidate all teams, knowledge and resource into one central hub, whilst being able to effectively cover the whole of the UK and beyond.

Stancold 2000
2001

From father to son

Mervyn Gillham retires at a young age to a warm country with a cold beer. His son, Kevin Gillham, takes over as Managing Director and remains to this day.

Stancold 2001
2002

Gilcrest Group

Gilcrest Group is established with a separate manufacturing division to provide specialist composite panels to the broader market whilst supporting Stancold's continued development.

Stancold 2002
2002-2015

Stronger team and offering

Stancold strengthens its team and offering to the market by introducing innovative uses of insulated panels for other applications such as firewalls. Throughout the recession, Stancold remained profitable and retains all the key personnel who make the business what it is. A core of staff at this time have been in the same business for 20 years.

Stancold 2002-2018
2015-2020

Cleanroom Development

Demonstrating resilience amidst Brexit uncertainty and a worldwide pandemic, Stancold preserves its strong financial status and diversifies our offering further. Where we saw an increase in demand from clients for more technically challenging projects, including cleanroom envelopes and humidity-controlled facilities, a specialist team was formed within the business.

Stancold 2005-2020
2021 – 2025

Complex Project Delivery

Stancold increasingly demonstrates design-and-build envelope solutions for demanding applications across the UK, such as battery manufacturing facilities, nuclear establishments and major pharmaceutical expansion projects.

Stancold Present
Present

Strength to Strength

Ahead of the next stage of strategic growth and investment, the company restructures, introducing Chris Honer as CEO, supported by a Senior Management Team that aligns expertise across every stage of the customer journey. This reflects a clear intent to build on strong foundations, sector diversification and continued investment in people, innovation and operational strength.

ACCREDITATIONS

Back Next
Accreditation

BRE - UKAS; ISO 9001:2015

BRE Global provides independent, third-party certification of fire, security and environmental products and services. ISO 9001:2015 ensures that our customers get consistent, good quality products and services.

Accreditation

SafeContractor

The SafeContractor scheme is designed to review and audit the health and safety policies, procedures and documentation of contractors giving our clients continued piece of mind.

Accreditation

LPS 1500

This standard defines the requirements for companies installing fire resisting compartment systems approved by LPCB to the requirements of LPS 1208 – LPCB fire resistance requirements for elements of construction used to provide compartmentation.

Accreditation

Constructionline

Constructionline is the UK’s leading procurement and supply chain management service that provides efficiency savings by reducing risk, creating cost efficiencies and helping buyers engage with new suppliers.

Accreditation

CHAS Accredited Contractor

CHAS is a pre-approval scheme run by the Government assessing suppliers' conformity with Health and Safety laws. It saves both time and resources for buyers when looking for the right supplier.

Accreditation

Cold Chain Federation

The voice of the temperature-controlled supply chain in the UK, the federation is the leading source of information, advice and guidance for businesses within the industry.

Accreditation

FPA

The Fire Protection Association (FPA) is the UK's national fire safety organisation who work to and identify the dangers of fire and the means by which their potential for loss is kept to a minimum.

Accreditation

Builder’s Profile

Gives main contractors the opportunity to receive our up-to-date pre-qualification profiles and gives confidence that your supply chain is up-to-date and meets your insurance and health and safety responsibilities.

Accreditation

BSG Membership

BSG help us minimise the risk of accidents in the workplace and keep us up to date and compliant with all health, safety and environmental regulations.

Accreditation

Taste of the West

We are proud to support Taste of the West, a unique membership organisation for food and drink businesses across the South West. Stancold are Taste of the West's Preferred Partner for Food Factory Fit-Out.

Accreditation

Taste of the West Awards Sponsor

In line with our goal to support food and drink producers in the South West, we are very pleased to be sponsors of the 2025 Taste of the West Awards.

SOME OF OUR CLIENTS

Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo
Client logo

Products & Services

  • Food Facility Fit-Out
  • Cold Store Construction
  • Cleanroom Construction Solutions
  • Firewalls & Industrial Partitions

Pages

  • Our Team
  • Case Studies
  • News
  • Privacy Policy
  • Stancold: Insurances

Location

0117 316 7000
info@stancold.co.uk

Accounts: accounts@stancold.co.uk
Company Registration Number: 00425982
© Stancold PLC

Stancold PLC
Portview Road
Avonmouth, Bristol
BS11 9LQ
United Kingdom

Stancold