Background:
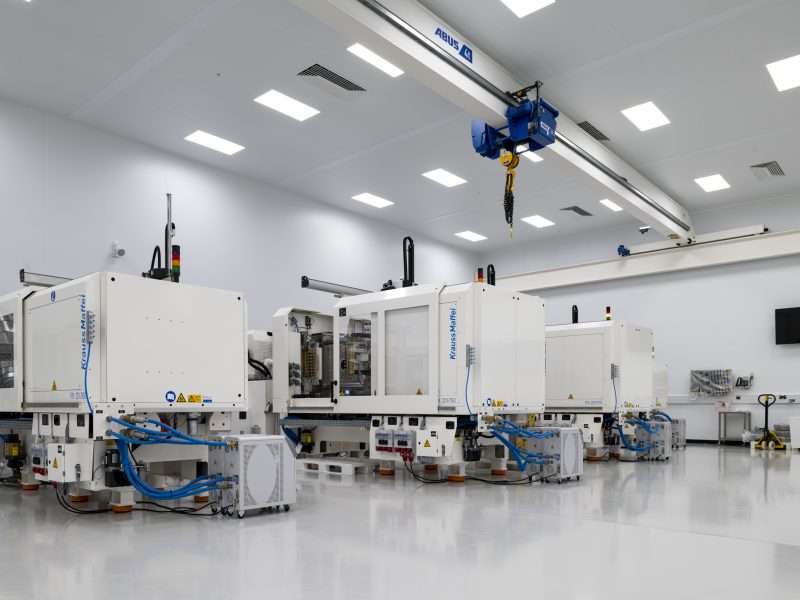
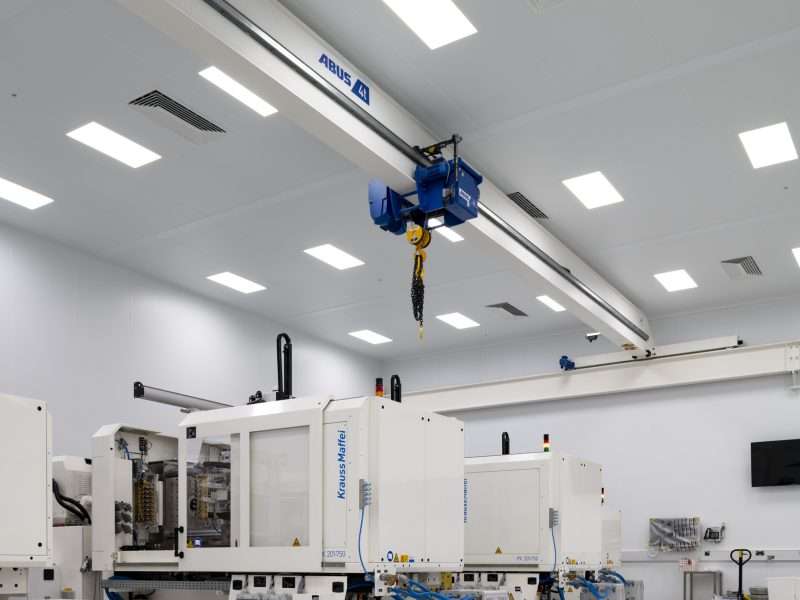
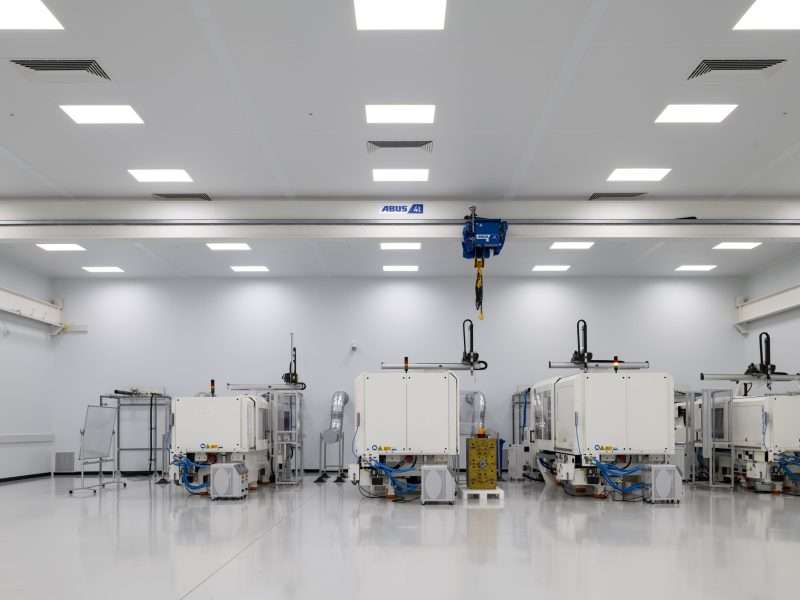
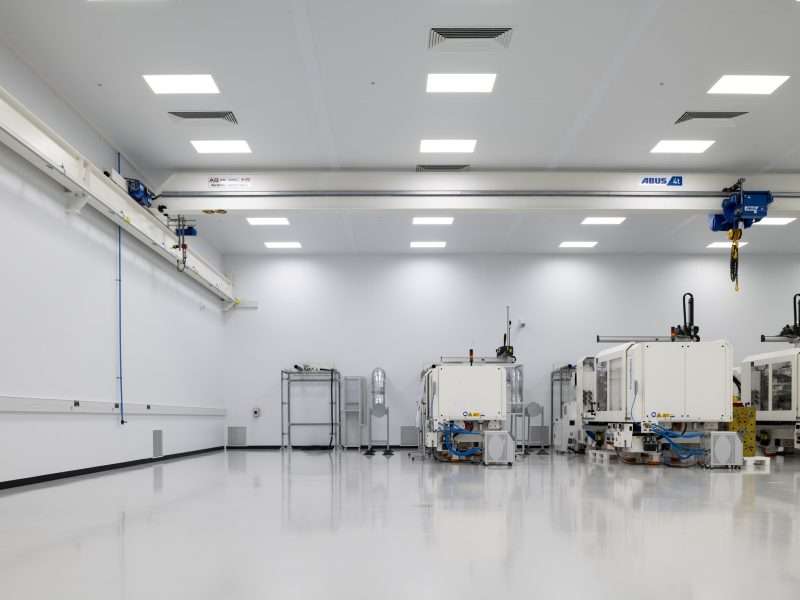
As a result of our expertise and bespoke cleanroom envelope packages, Stancold were awarded a new-build contract with a battery research organisation that specialises in reusing and recycling tin mining materials to create lithium batteries.
Process:
The client requested the new-build cleanroom as part of a pilot phase for a large-scale facility in the long-term.
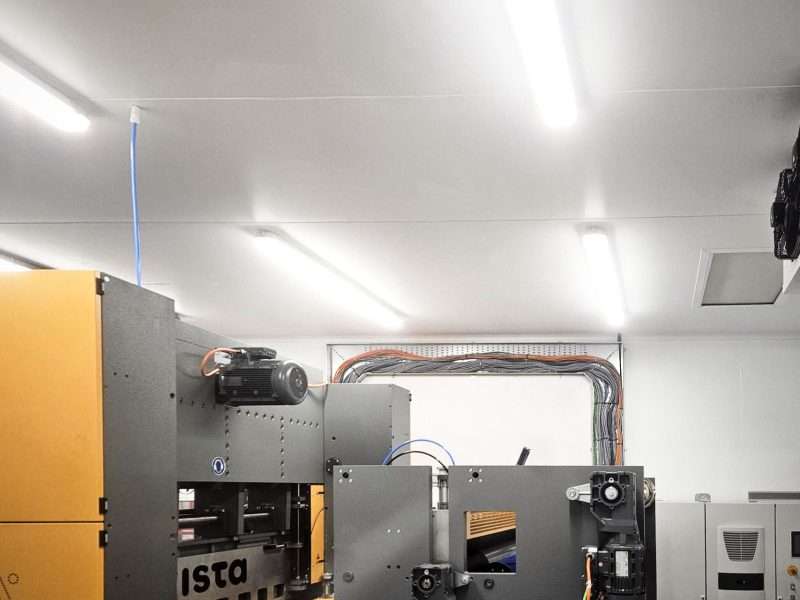
Throughout the contract, the team collaborated closely with the manufacturing equipment contractor, who would later install the new machinery.
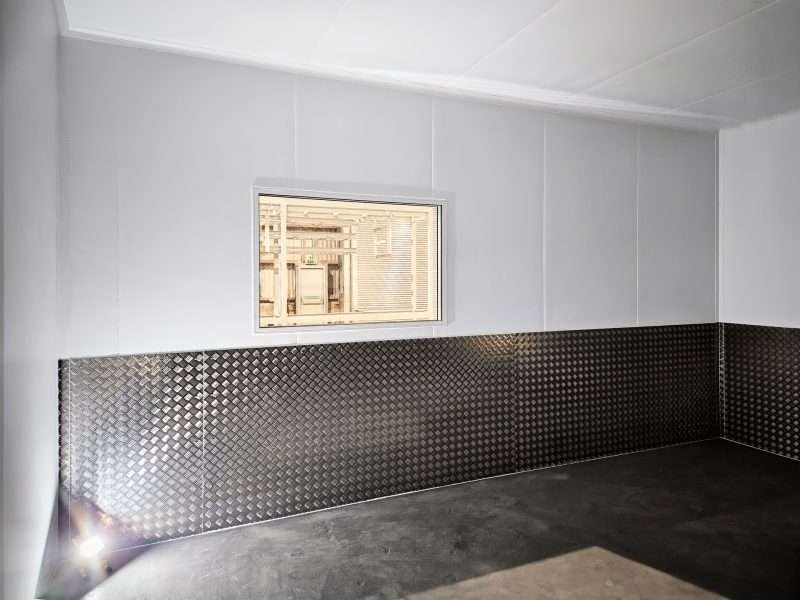
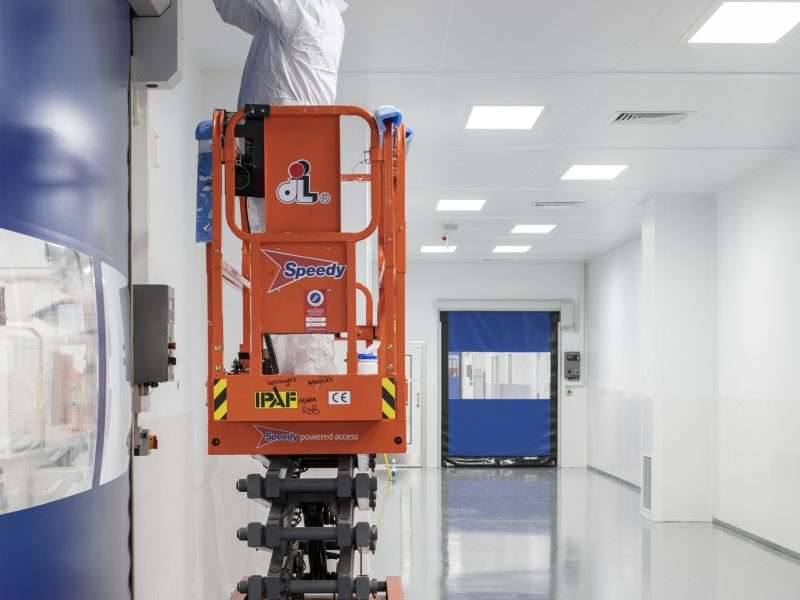
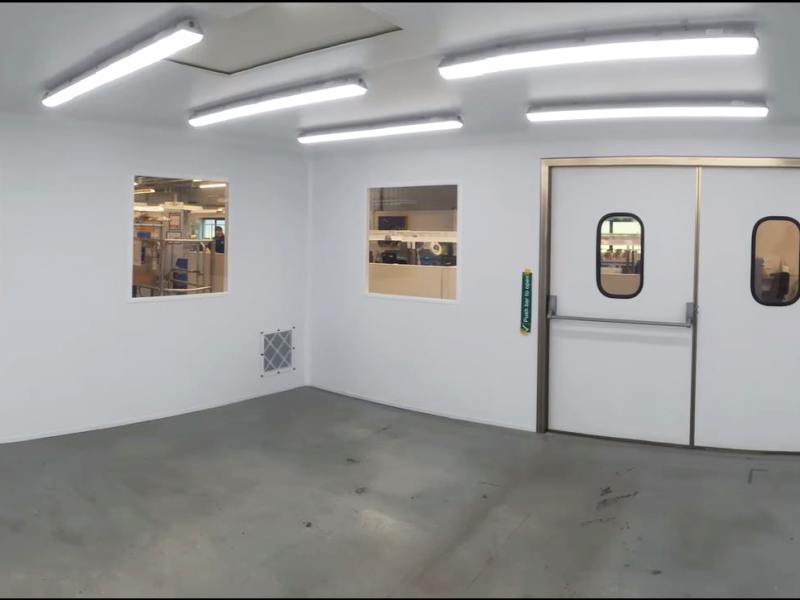
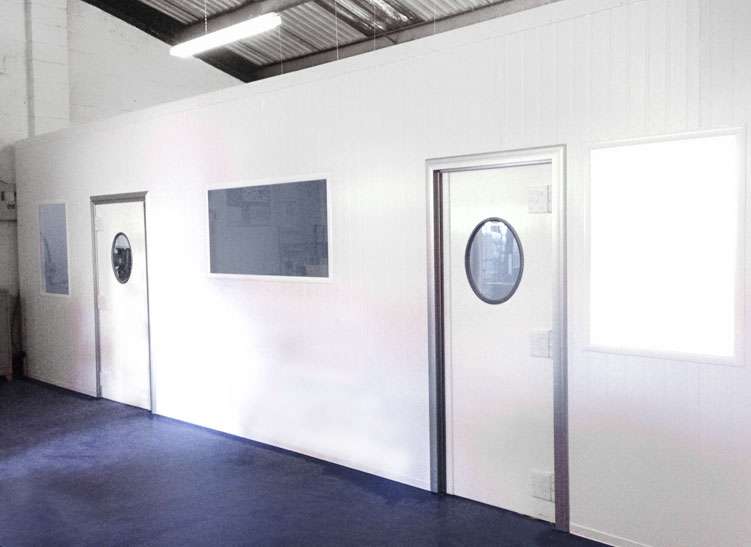
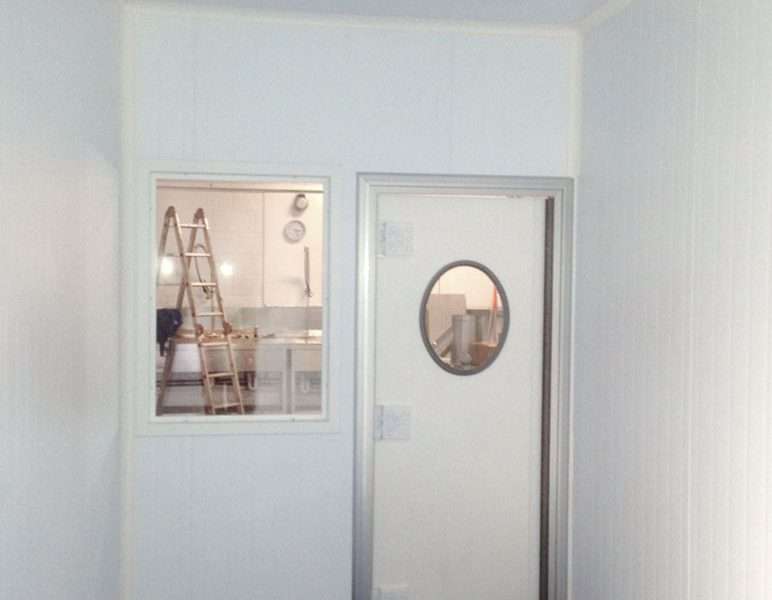
Included in the scope was the design and installation of double personnel doors for ease of access and a vision panel to enhance visibility within the facility.
Project Delivery:
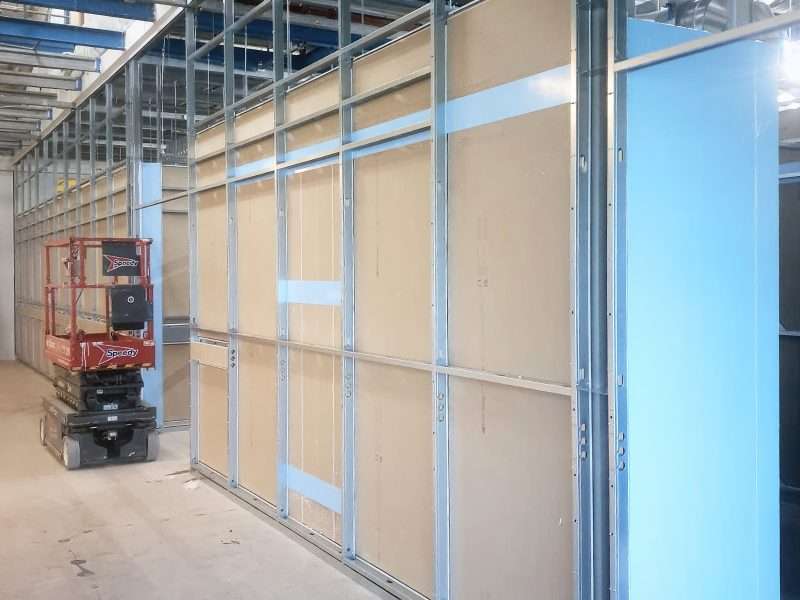
The team’s flexibility and proactive nature allowed them to build the initial walls during the first site visit, leaving a pre-designed opening to allow for the manufacturing equipment to be installed.
Due to the nature of the client’s work, a phased installation was required. The second phase began once the new equipment had been installed, resulting in the team returning to seal the room.
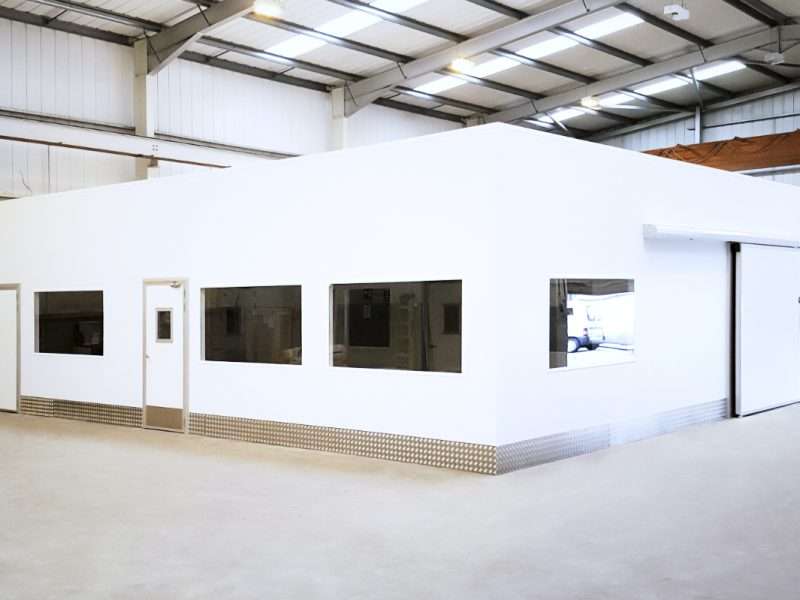
As per the client’s request, the team installed treadplate wall protection across the cleanroom perimeter in order to minimise the risk of potential damages.
The teams’ flexibility in this project left the client satisfied with the results.