The Brief
Stancold were involved in early-stage negotiations with a growing speciality food wholesaler, who were looking to expand and relocate their manufacturing facility within Birmingham.
Experienced project management contractor, Pentadel, took on the full turnkey package to transform and extend an existing building into a fit-for-purpose food manufacturing facility.
Our Approach
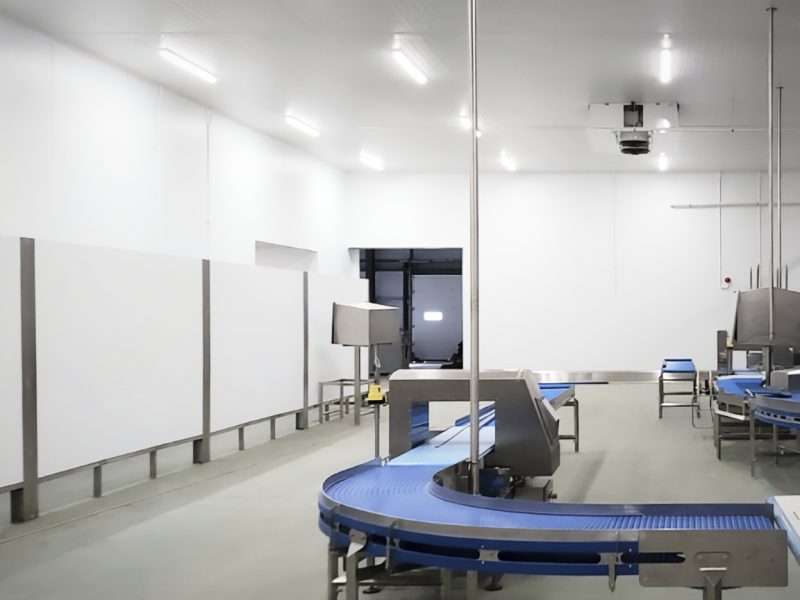
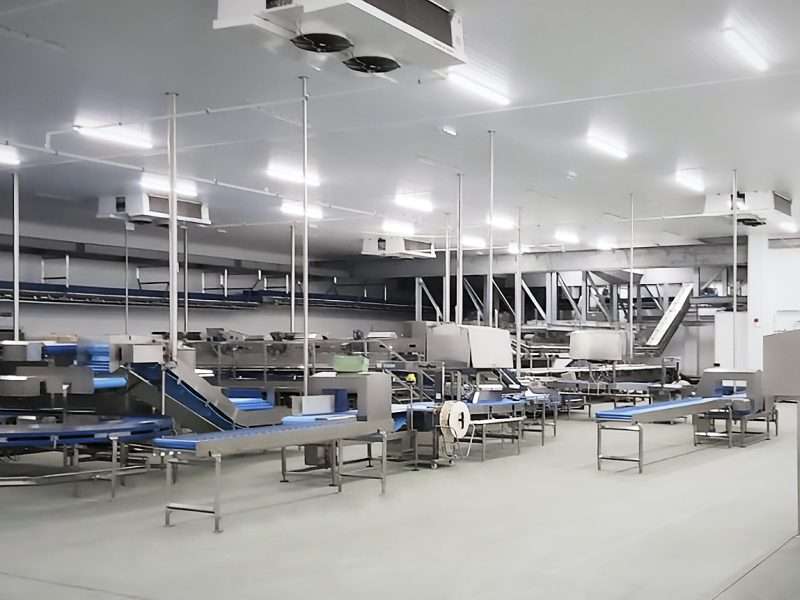
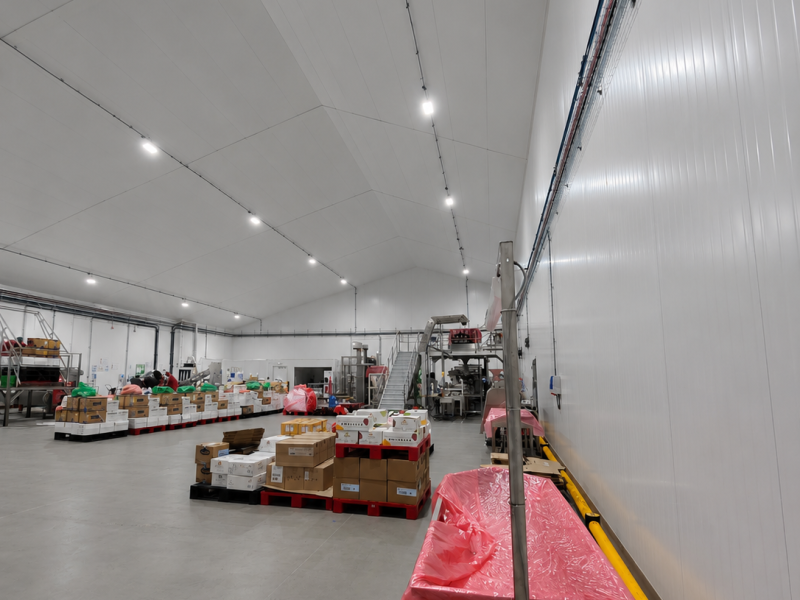
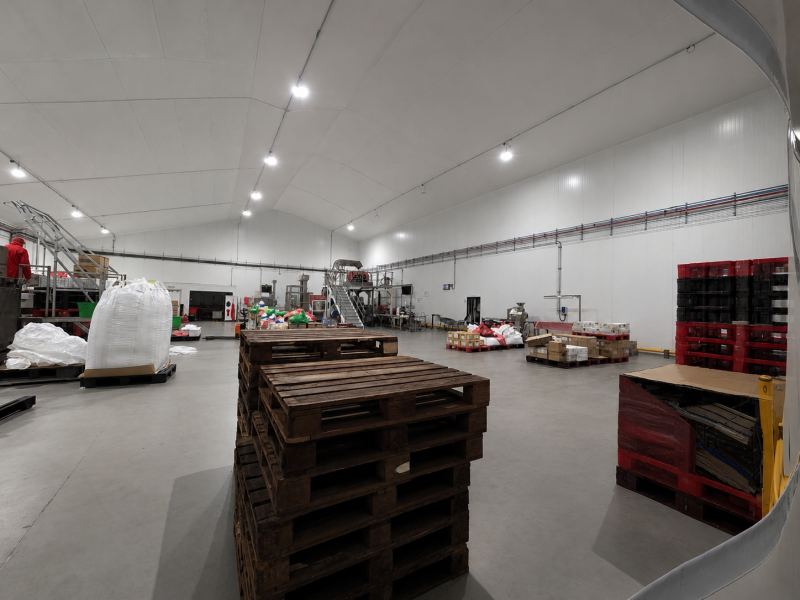
Stancold were appointed to undertake the food facility’s internal fit-out, alongside the internal and external cladding of a purpose-built extension, suited to product packaging and dispatch.
Our team worked collaboratively on the design and specification of this project to ensure that the end user’s requirements were met. Transferring specialist panel-build knowledge and skills into the external extension works allowed us to confidently add this element to our responsibilities.
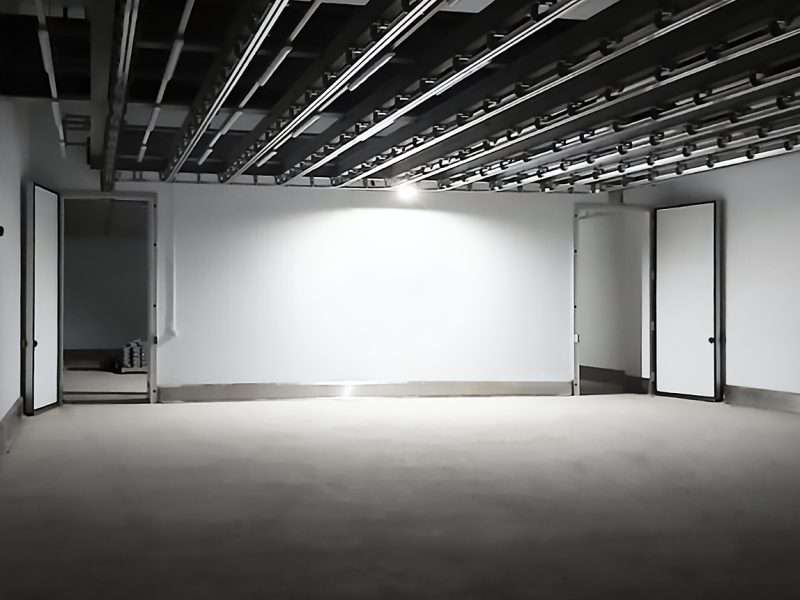
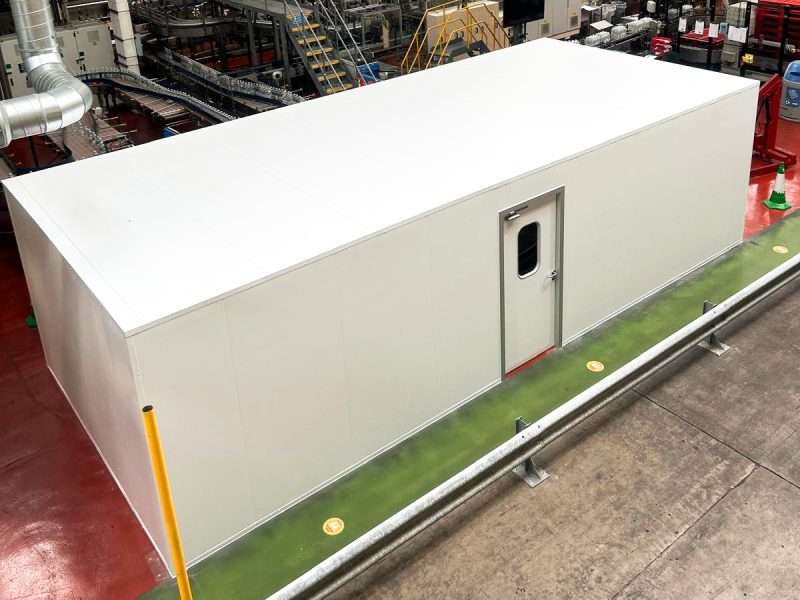
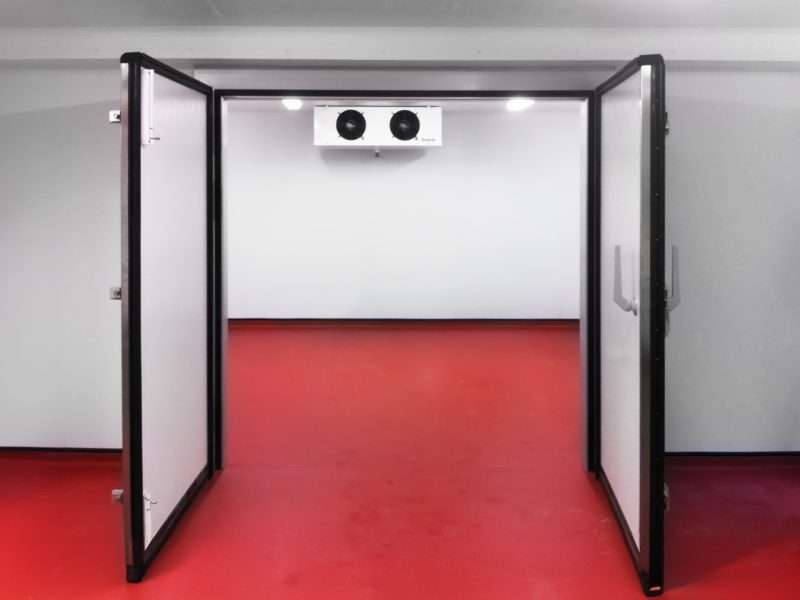
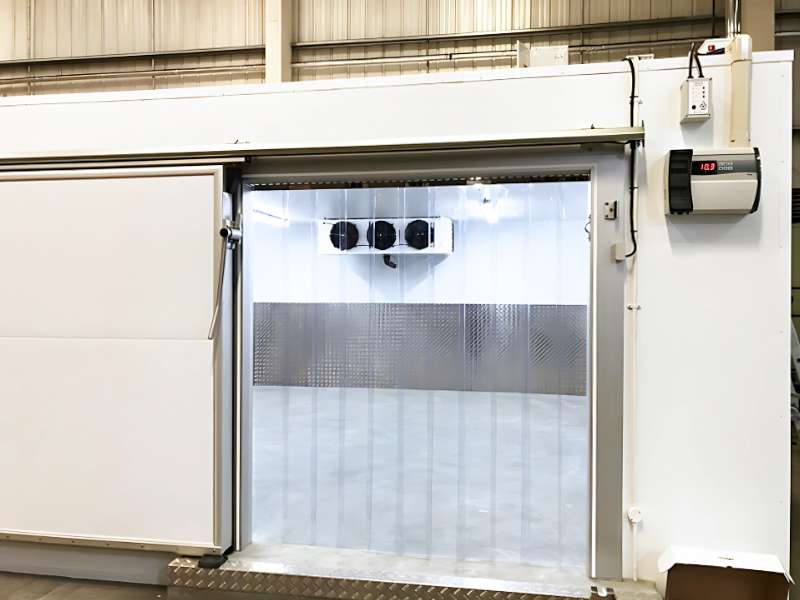
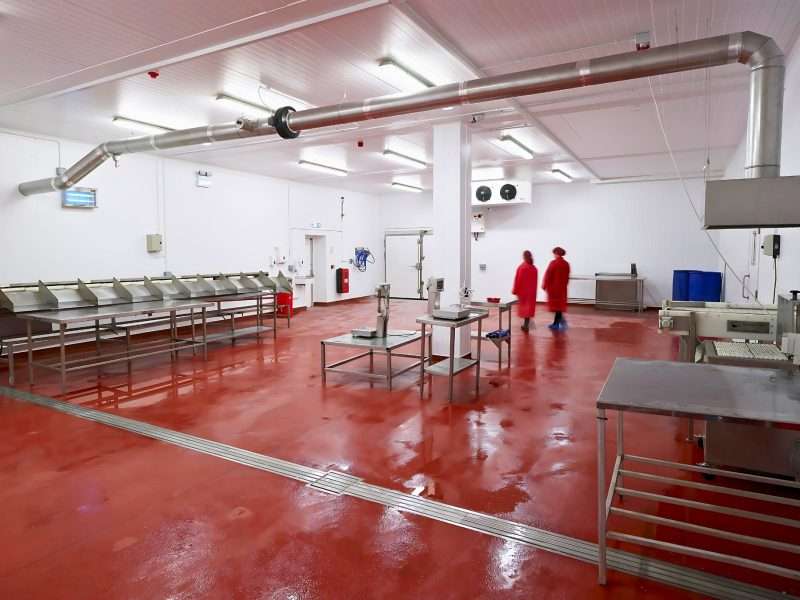
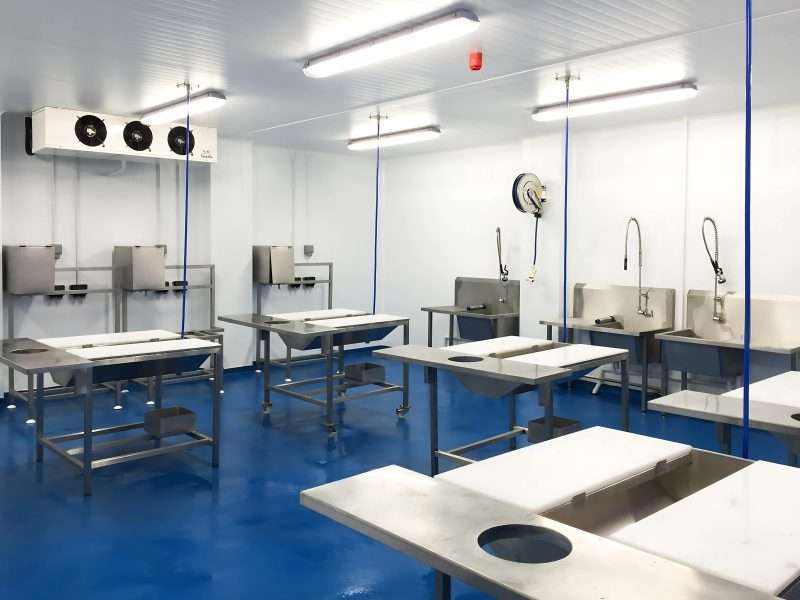
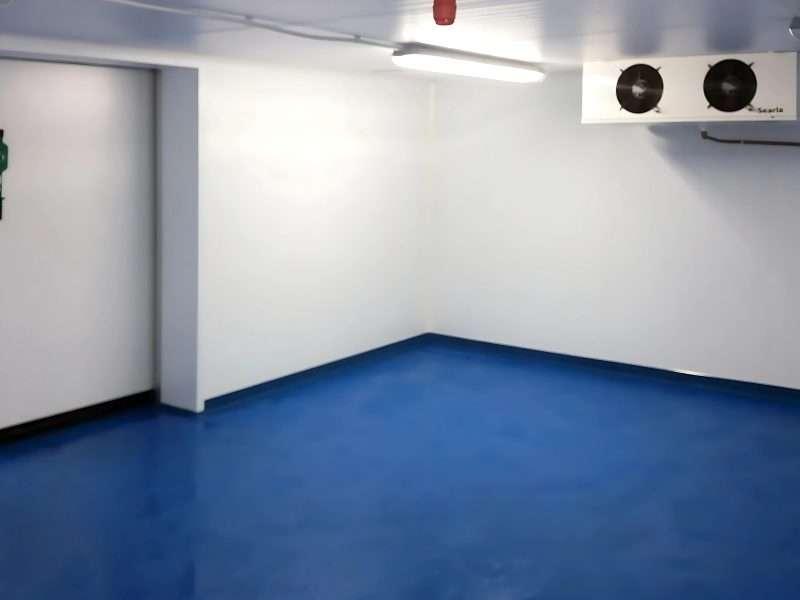
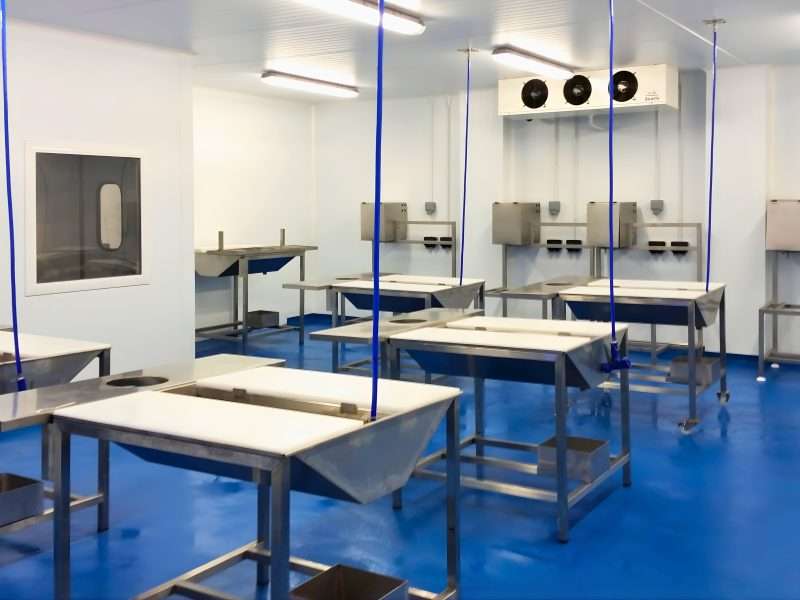
The full specification included over 10 different areas, such as main production, a blast chiller, a dry store and a soy room.
Delivery in Action
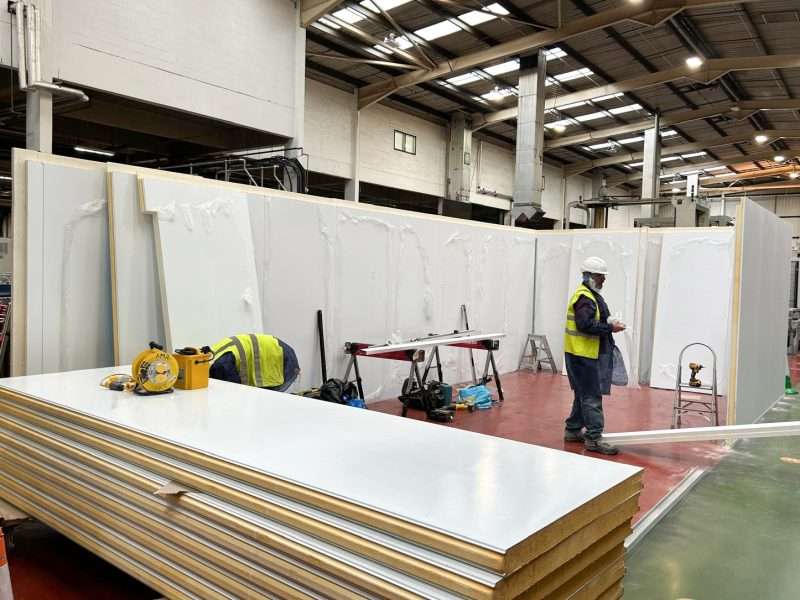
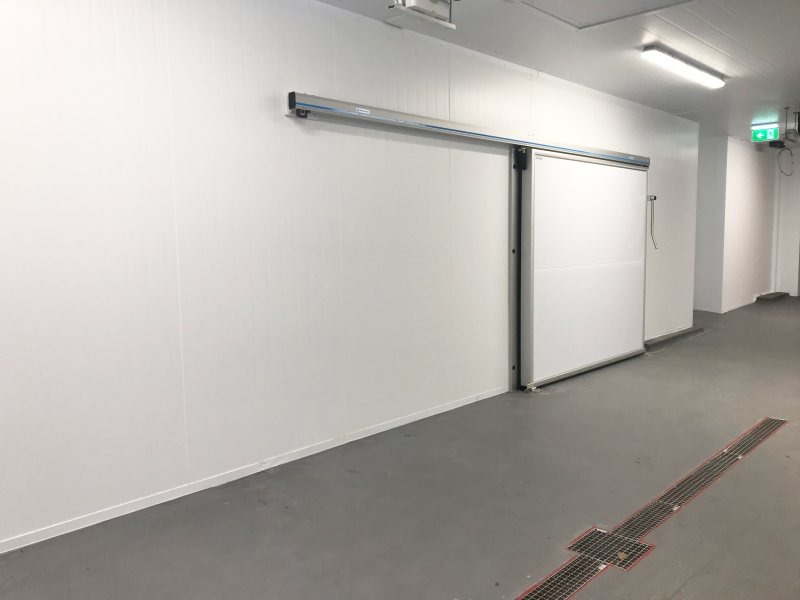
As part of a 9-month phased construction, which included coordinating with other contractors on the busy site, Stancold successfully completed the hygienic panel installation to form areas as per the end user’s specification, alongside a 60-minute sub-dividing firewall between the building and its new extension, another part of Stancold’s scope to meet fire safety building regulations.
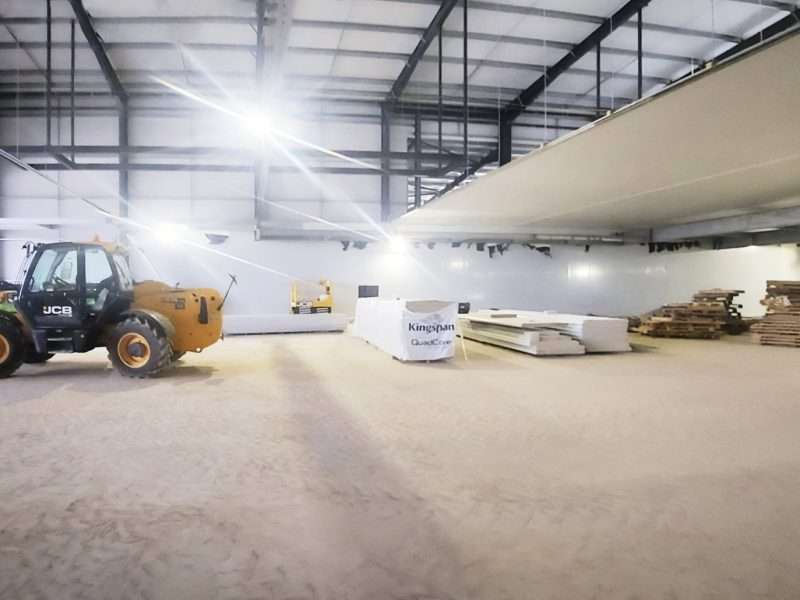
The internal fit-out extension construction included all cladding, using goosewing grey trapezoidal panels from Kingspan’s roof system, and door canopy. These works also encompassed a one-hour fire-rated boundary wall, utilising a RockSpan composite core. With tight access to consider, panels were craned from a bank to the rear of the building, alongside narrow plant used throughout.
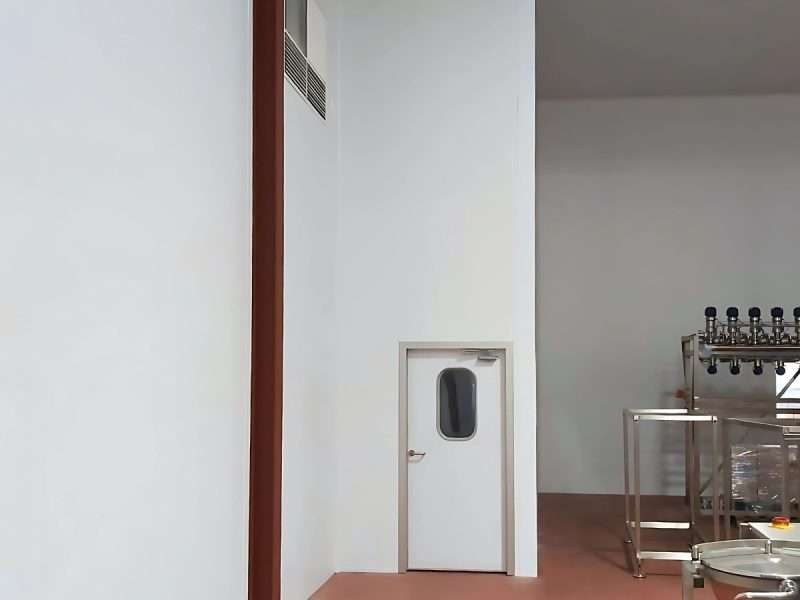
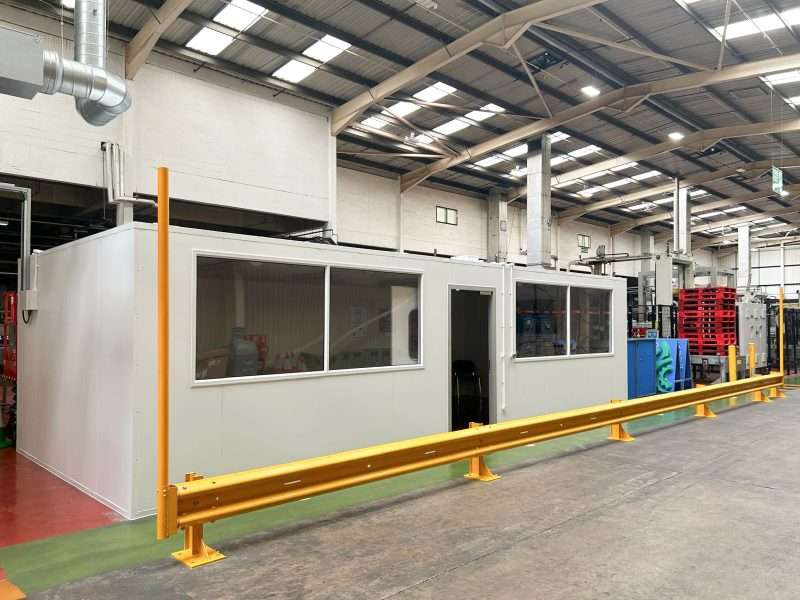
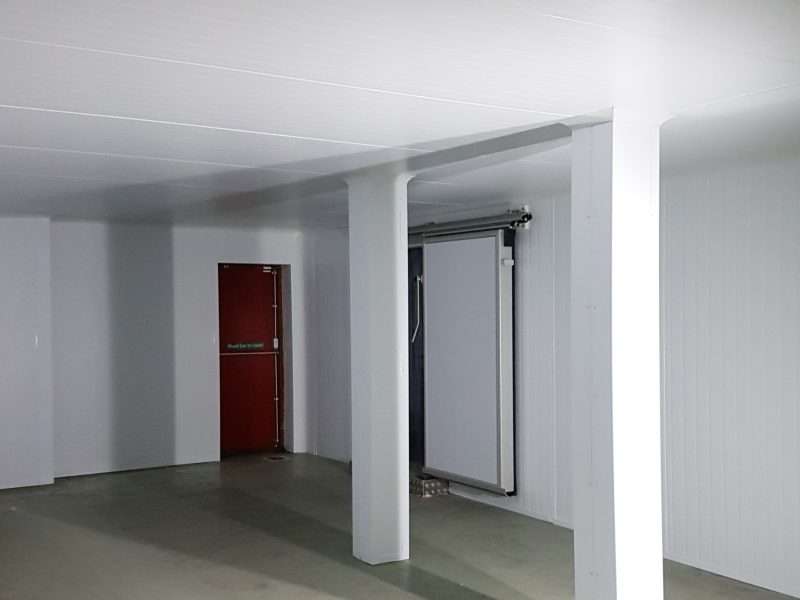
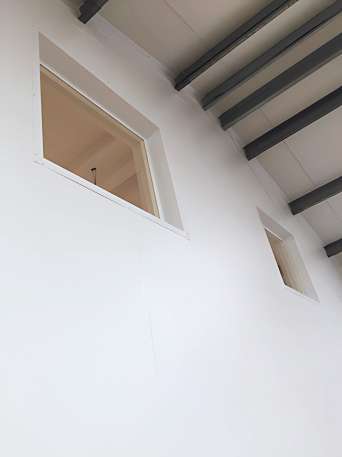
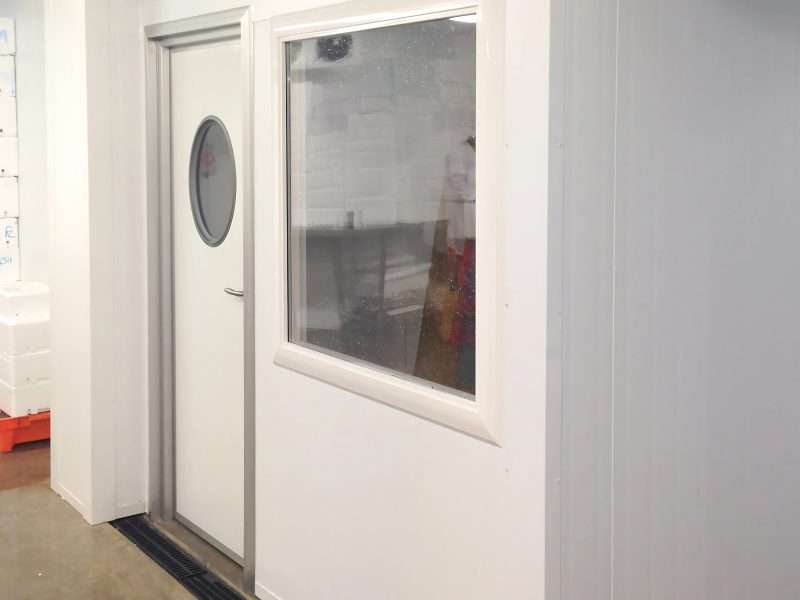
Internally, the fit-out incorporated bespoke window details to accommodate the building’s existing roof lights, as well as specialist flush windows, allowing free viewing into the main production area. The team constructed a bulkhead to neatly conceal air handling equipment and all existing steelwork was encased to maintain food safety excellence.
This was a large project that required timely planning and coordination at every stage, where our team thrived in demonstrating such qualities.
You can take a tour around the facility here.
A project that demonstrated our commitment to the food industry